Aluminium castings · no mould, no tooling charge鋁合金鑄件 · 不開模具、無模具費
A real casting, in your production alloy, before you spend anything on tooling. 在開模之前,先鑄一件真的出來。
A die-casting tool costs six figures and takes 90–120 days. We pour your part in the same alloy, by a casting process — from a 3D-printed pattern, with no tooling at all — so you find the shrinkage, the misrun and the thin-wall fill before the steel is cut. 一套壓鑄模動輒數十萬、等上 90~120 天。我們用同一種合金、以鑄造製程把你的件澆出來 —— 白模 3D 列印,完全不開模 —— 讓你在切鋼料之前就看到縮孔、冷隔與薄壁充填。
Aluminium poured into a fired ceramic shell. Footage from our production partner's foundry.鋁液澆入已焙燒的陶瓷殼型。畫面攝於合作產線。
A machined prototype is the wrong material in the wrong condition. 切削樣品的材料狀態,跟你的量產件不一樣。
Every fast prototyping route gives you a part that looks right. None of the usual ones give you a part that solidified like your production part will — and solidification is where casting defects come from. 所有快速打樣的路線都能給你一個「看起來對」的件。但一般那幾條路,沒有一條給你的件是照量產那樣凝固出來的 —— 而鑄造缺陷全部出在凝固這一段。
What you usually get一般拿到的
- CNC from bar stock — wrought 6061/7075. No porosity, no shrink, no fill path. It cannot fail the way your casting will.
- CNC 從實心料切 —— 鍛材 6061/7075。沒有氣孔、沒有縮孔、沒有充填路徑。它不可能用你的鑄件會壞的方式壞掉。
- Metal 3D printing (SLM) — rapidly solidified microstructure, nothing like a sand or foam casting. And expensive.
- 金屬 3D 列印(SLM) —— 快速凝固組織,跟砂型或消失模完全不同,而且很貴。
- A soft tool — which is the exact spend you were trying to avoid.
- 開軟模 —— 那正是你想避開的那筆錢。
What we give you我們給的
- A casting. Poured into a ceramic shell, in your production alloy, with a real gate and riser and a real fill path.
- 一件真鑄件。澆進陶瓷殼型,用你的量產合金,有真的澆口與冒口、真的充填路徑。
- Section it, X-ray it, pull a tensile bar from it. If it is going to shrink, it shrinks here — on a part that cost you no tooling.
- 你可以剖開、可以照 X 光、可以從本體切試棒。要縮就在這裡縮 —— 縮在一件沒讓你付模具費的件上。
- Then change the geometry and we pour it again. Changing a printed pattern costs a file, not a die.
- 然後改幾何、我們再澆一次。改列印白模改的是一個檔案,不是一套鋼模。
Shell lost-foam, from a printed pattern.空殼消失模,白模用 3D 列印。
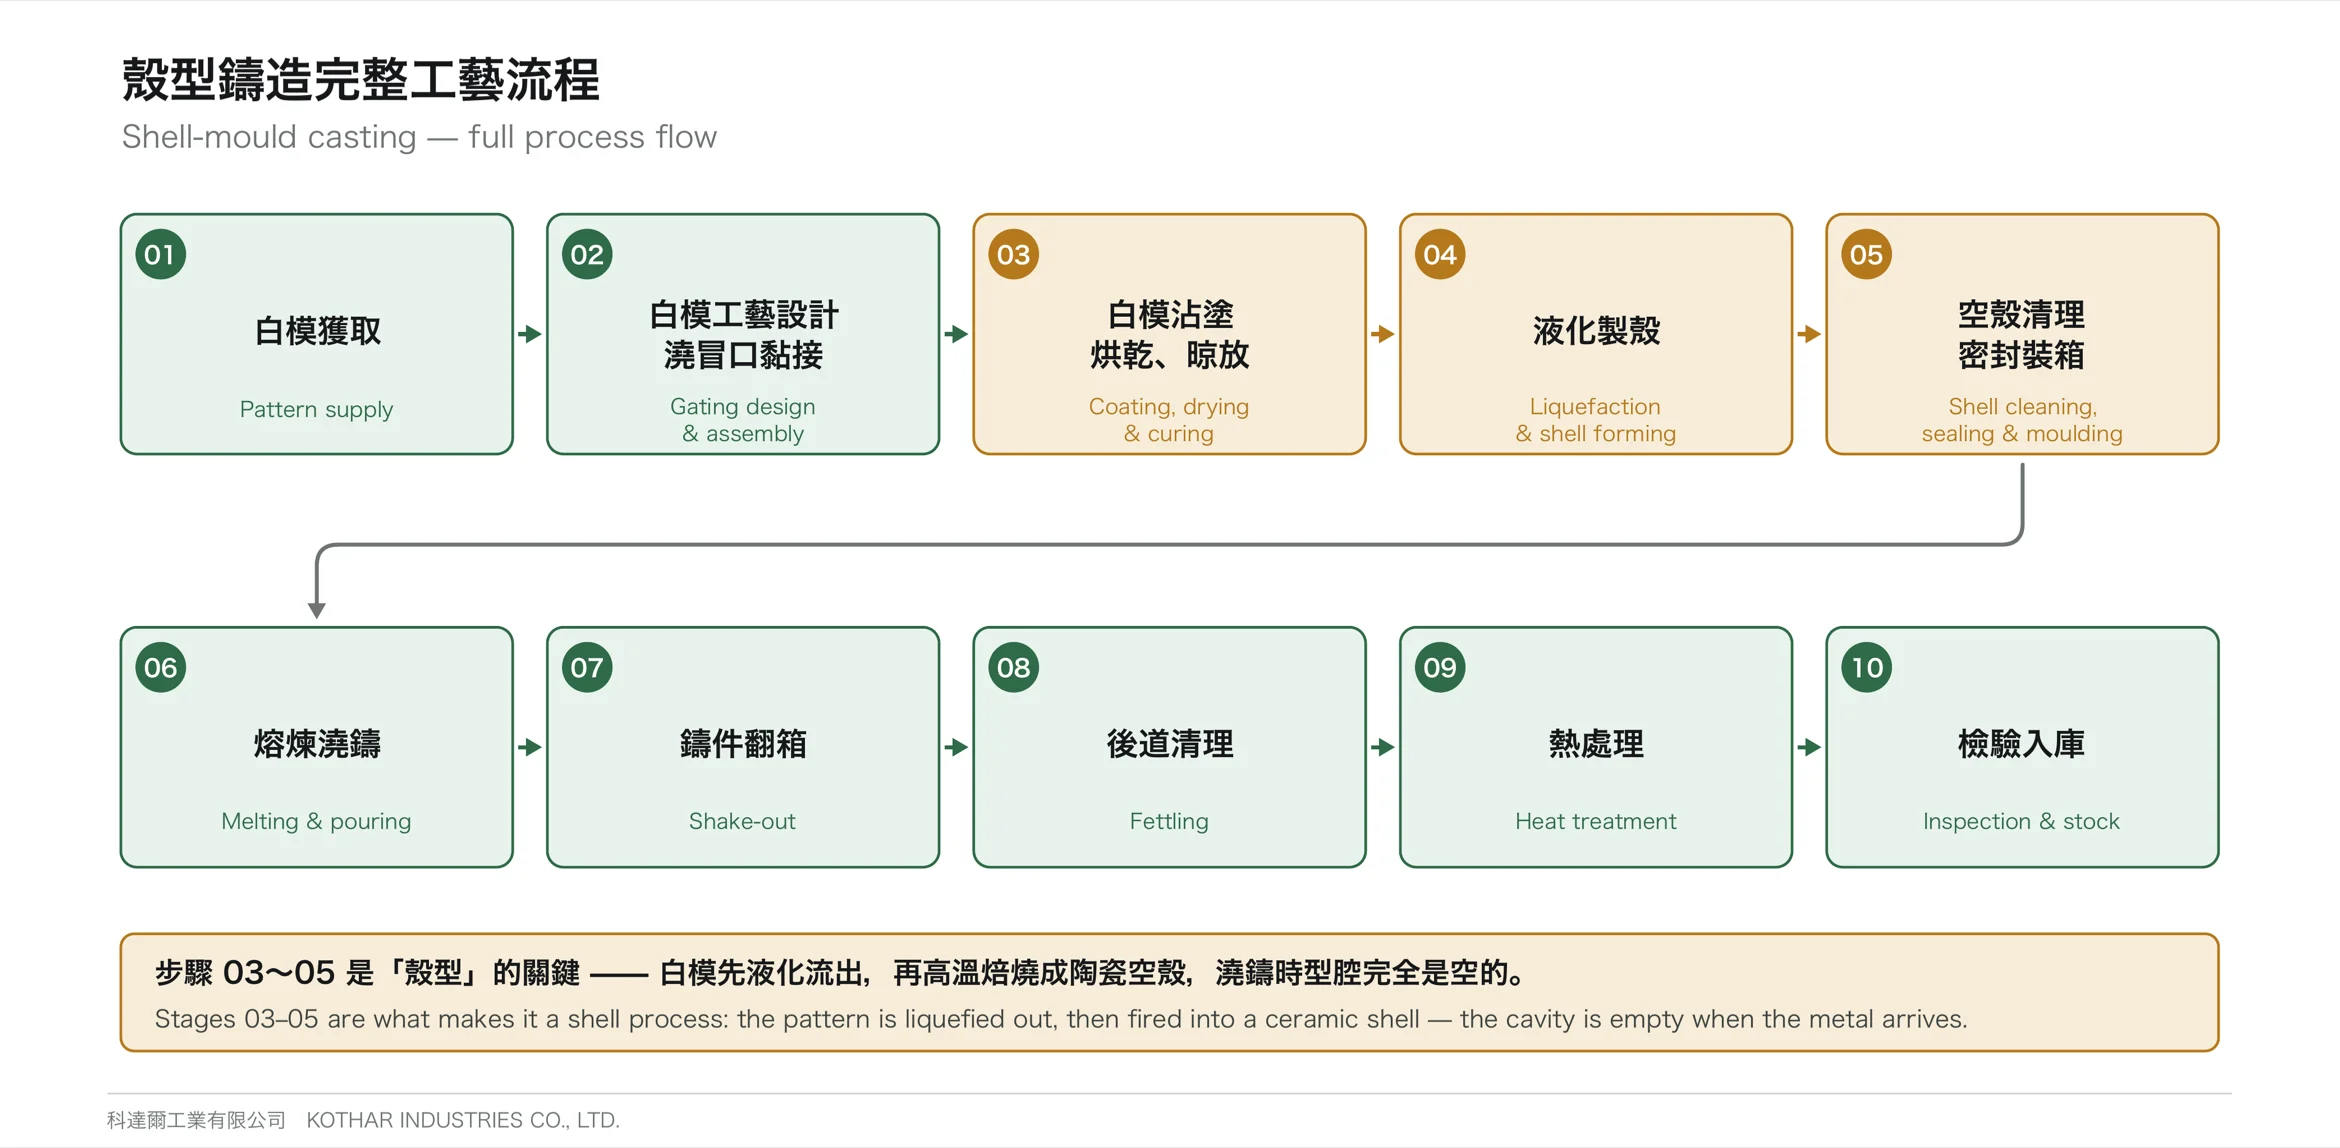
The pattern is printed, coated in refractory slurry, then burned out of the shell before pouring — so the cavity is empty when the metal arrives. No mould halves, no draft angles, no split lines to design around. 白模列印出來、掛上耐火塗料,在澆注之前就先燒失,所以金屬進去的時候型腔是空的。沒有上下模、沒有拔模斜度、沒有分模線要遷就。
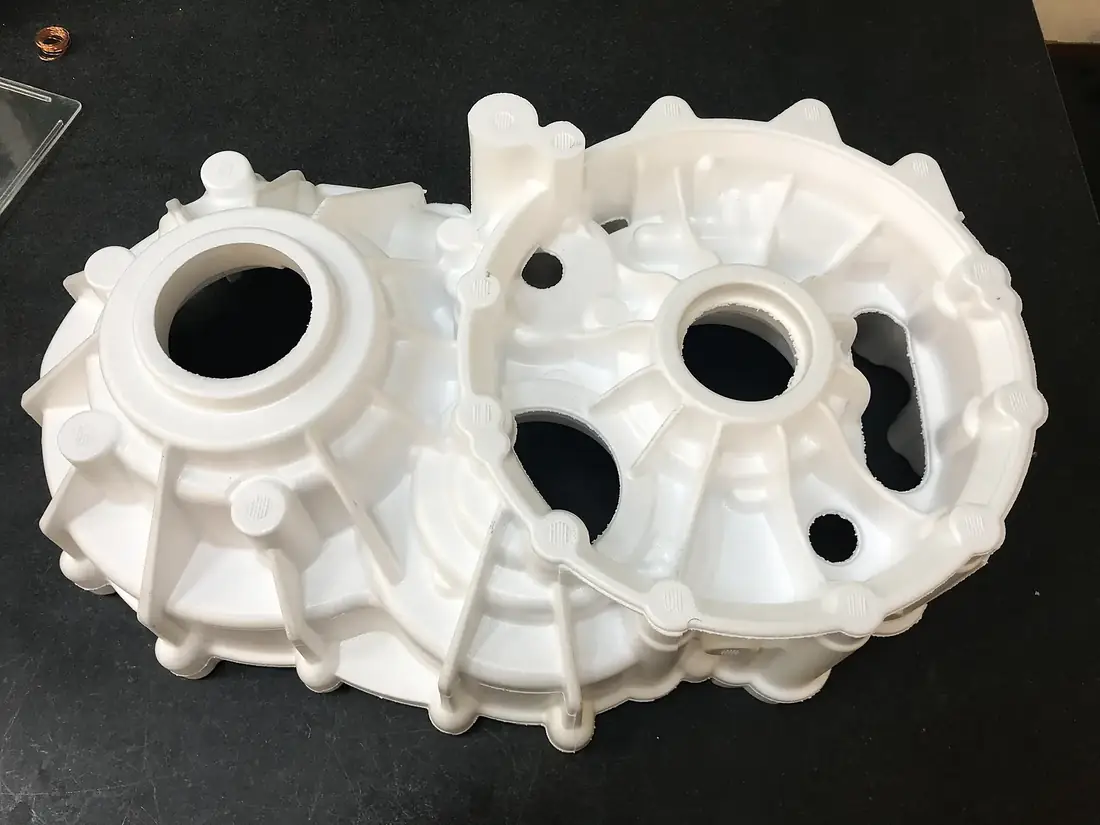
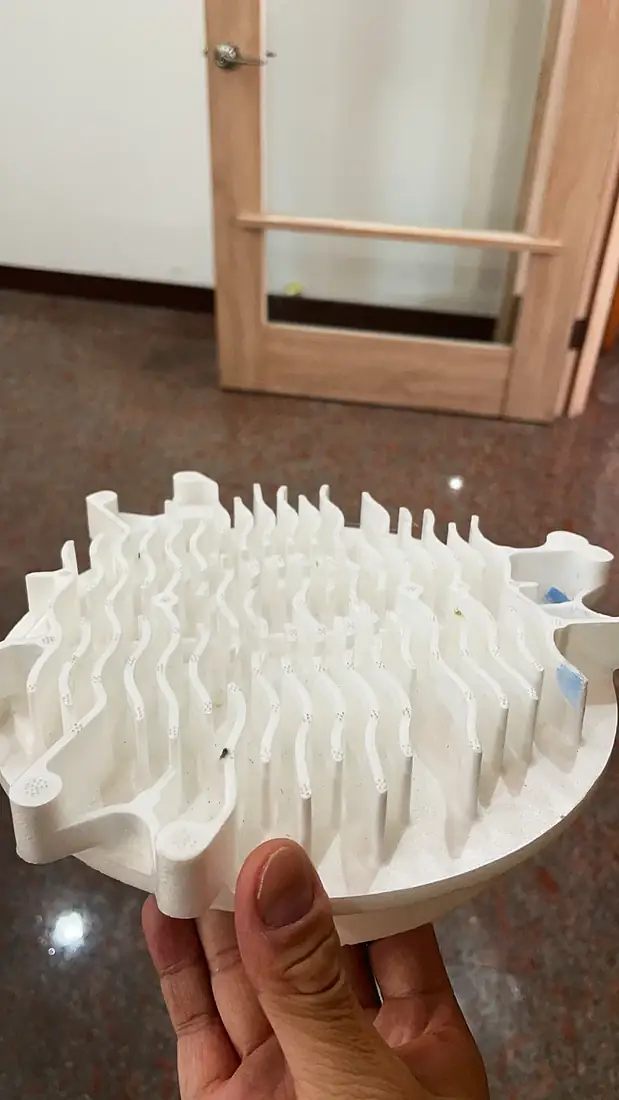
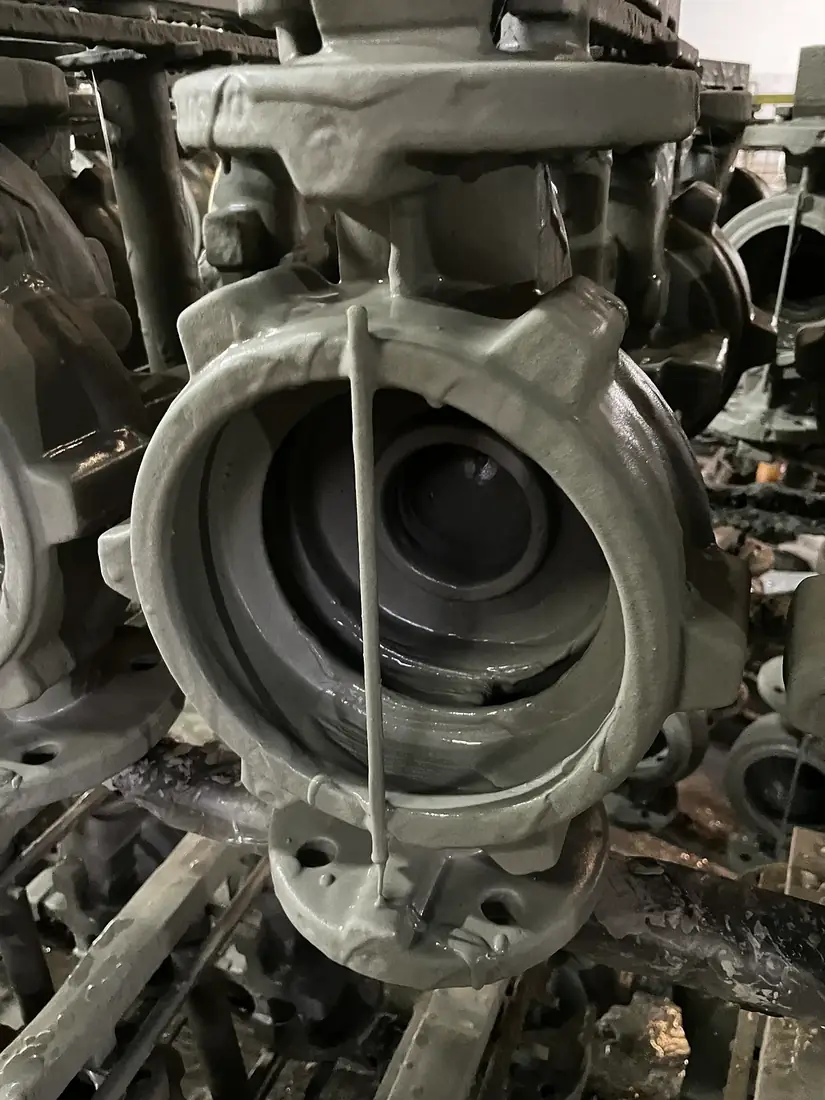
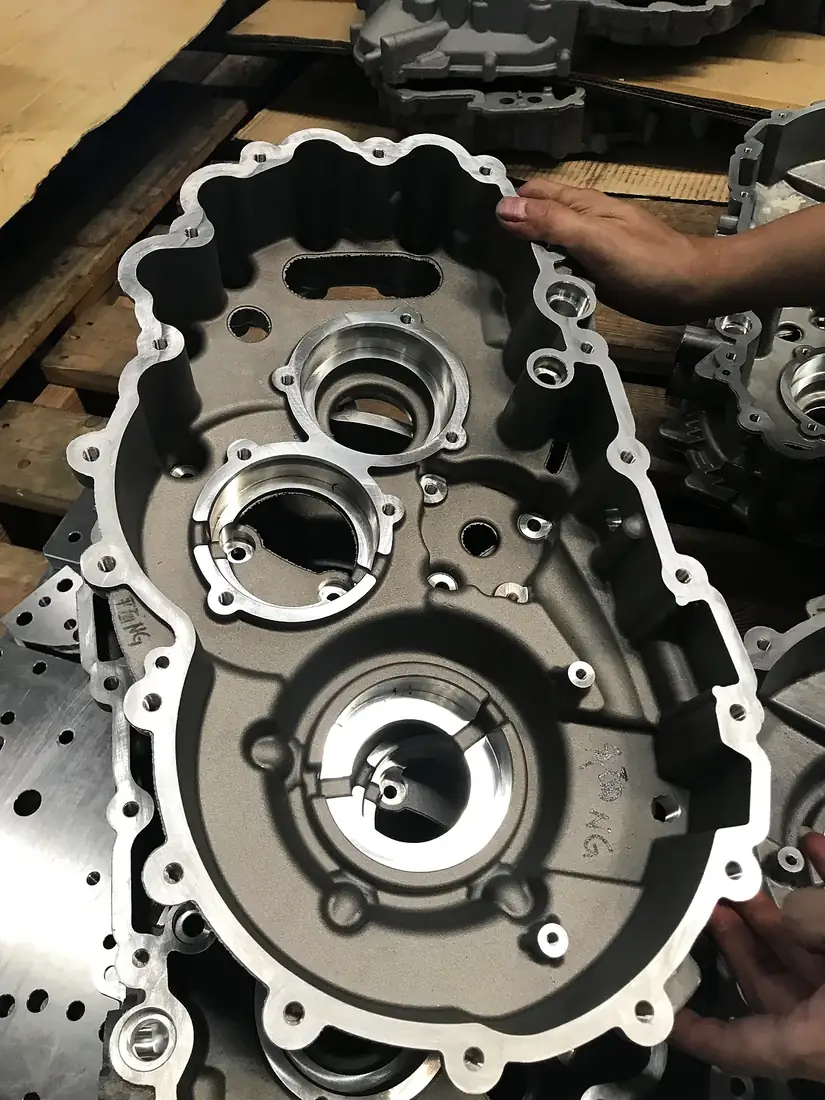
Pattern → shell → pour → part.白模 → 掛殼 → 澆注 → 成品。
Your file你的檔案
STEP or IGES. We review castability and come back within one working day.STEP 或 IGES。我們做可鑄性評估,一個工作日內回覆。
Gating design澆冒口設計
Gate, riser and feed path added to the pattern — the part of this that is twenty years of foundry judgement.在白模上加澆口、冒口與補縮路徑 —— 這一段靠的是二十年的鑄造判斷。
Pattern printed列印白模
Printed as one piece. Geometry changes cost a reprint, never a tool.一體列印。改幾何只是重印一支,永遠不動模具。
Shell & burnout掛殼與燒失
Refractory coating in layers, dried, then fired until the pattern is gone.耐火塗料逐層塗掛、乾燥,進爐燒到白模完全消失。
Pour澆注
A356.2 poured into the hot shell, then quenched and aged to T6.A356.2 澆入熱殼,之後淬火、時效到 T6。
Machine & ship加工與出貨
Datum faces, threads and critical dimensions machined. Door to door by courier.基準面、螺紋與關鍵尺寸加工完成。快遞門到門。
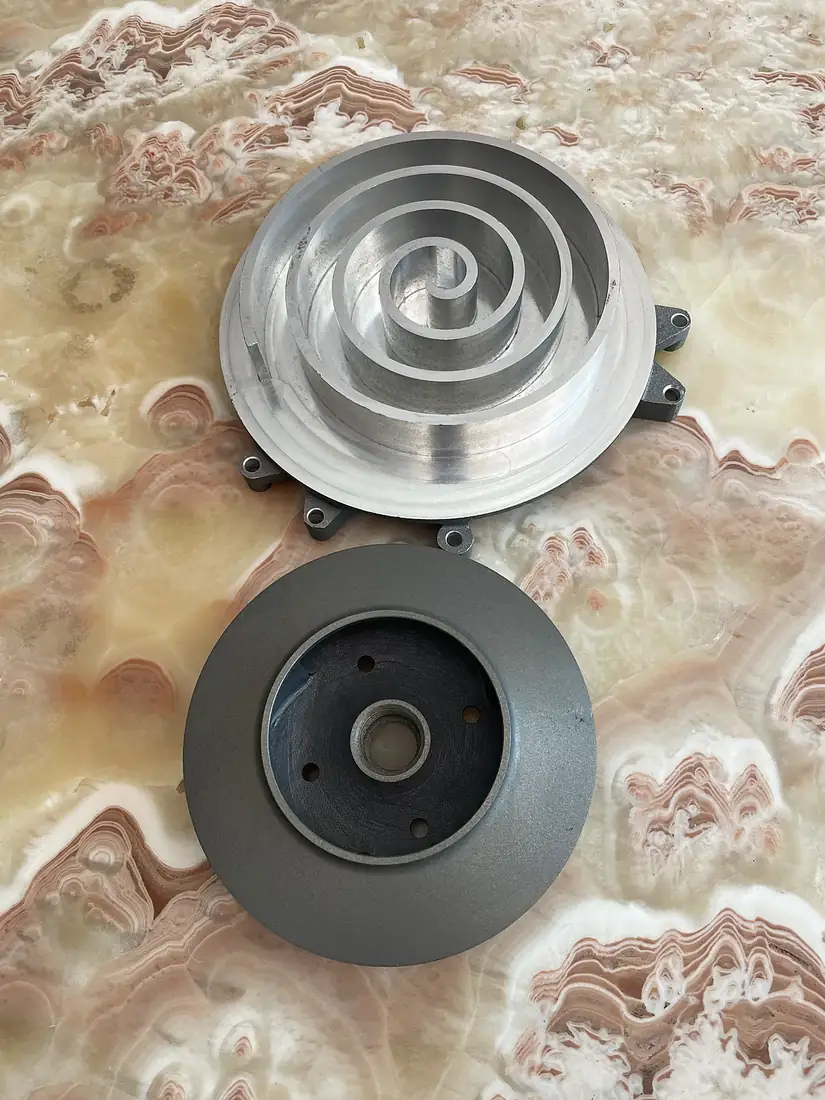
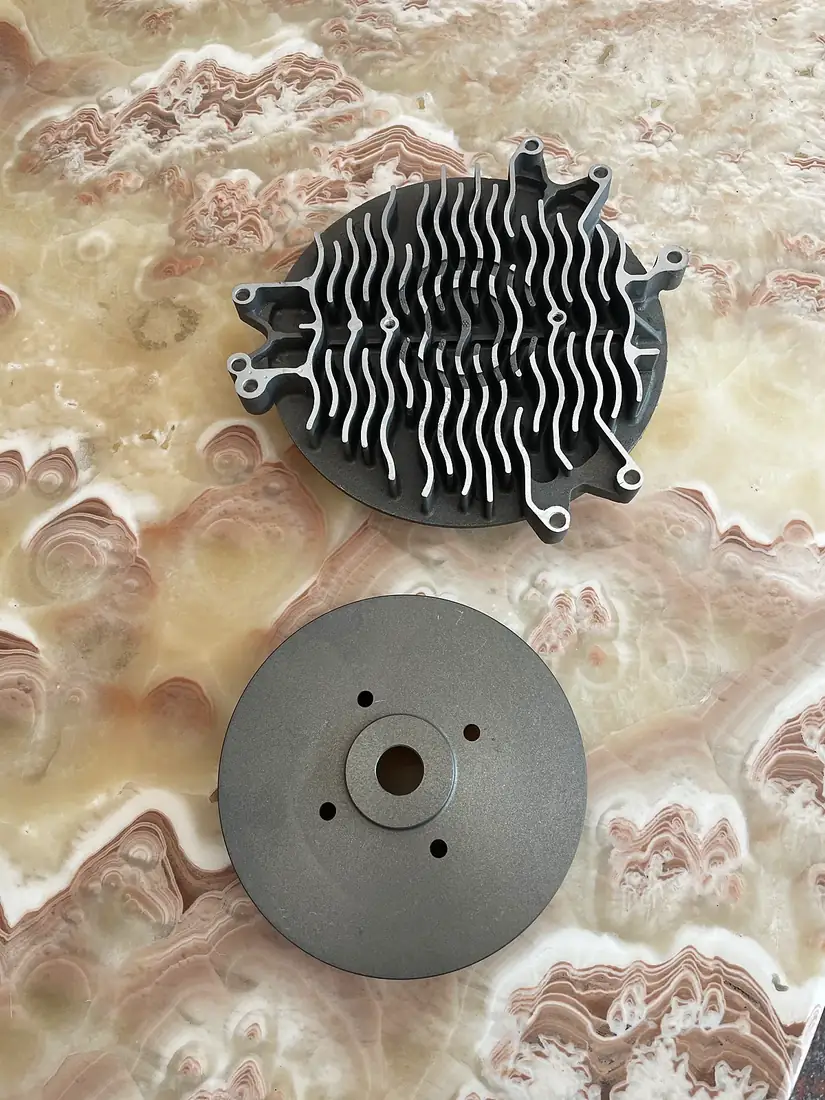
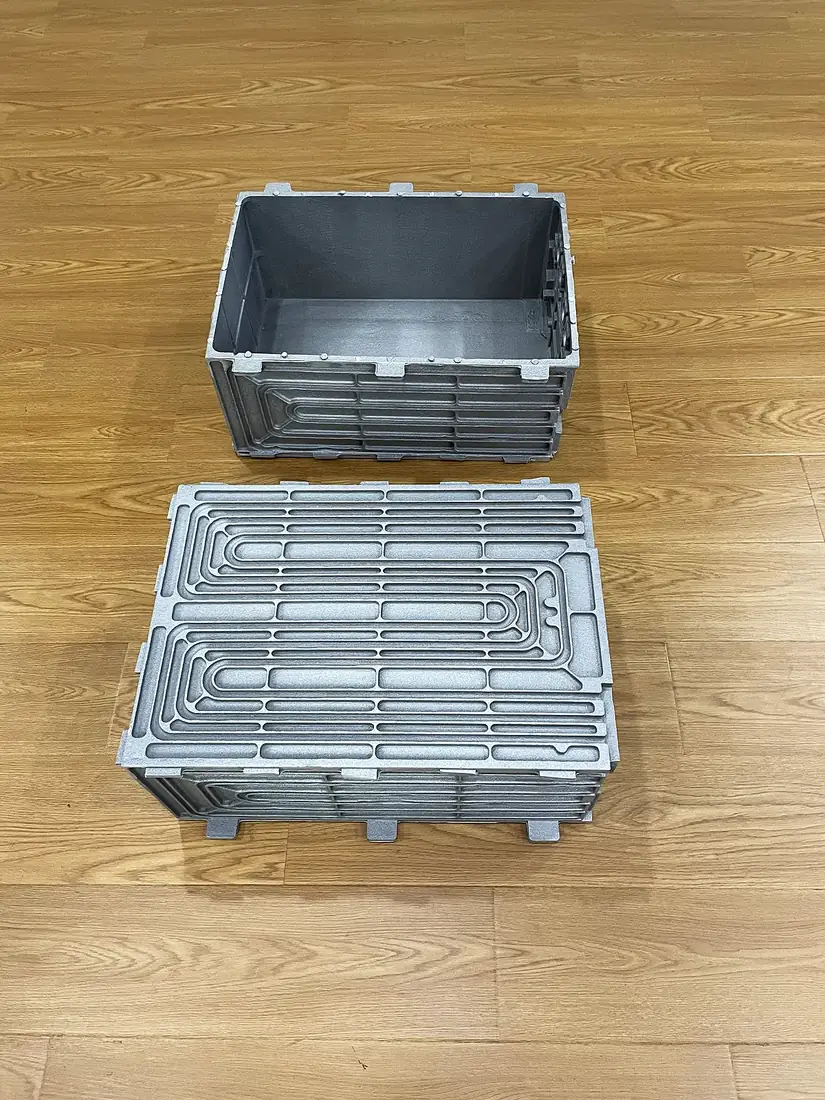
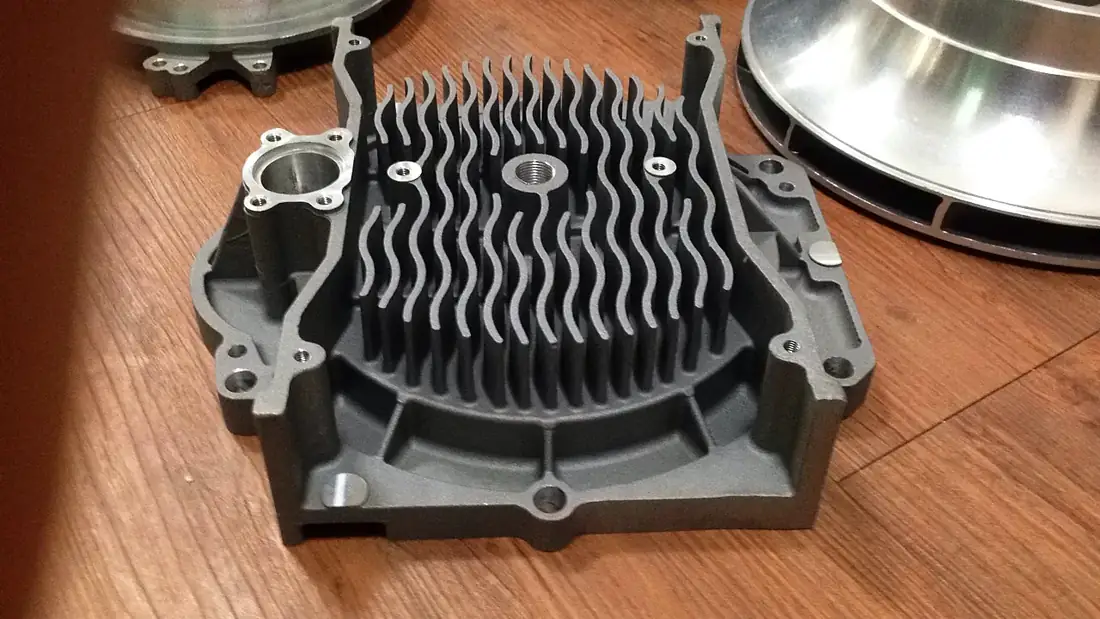
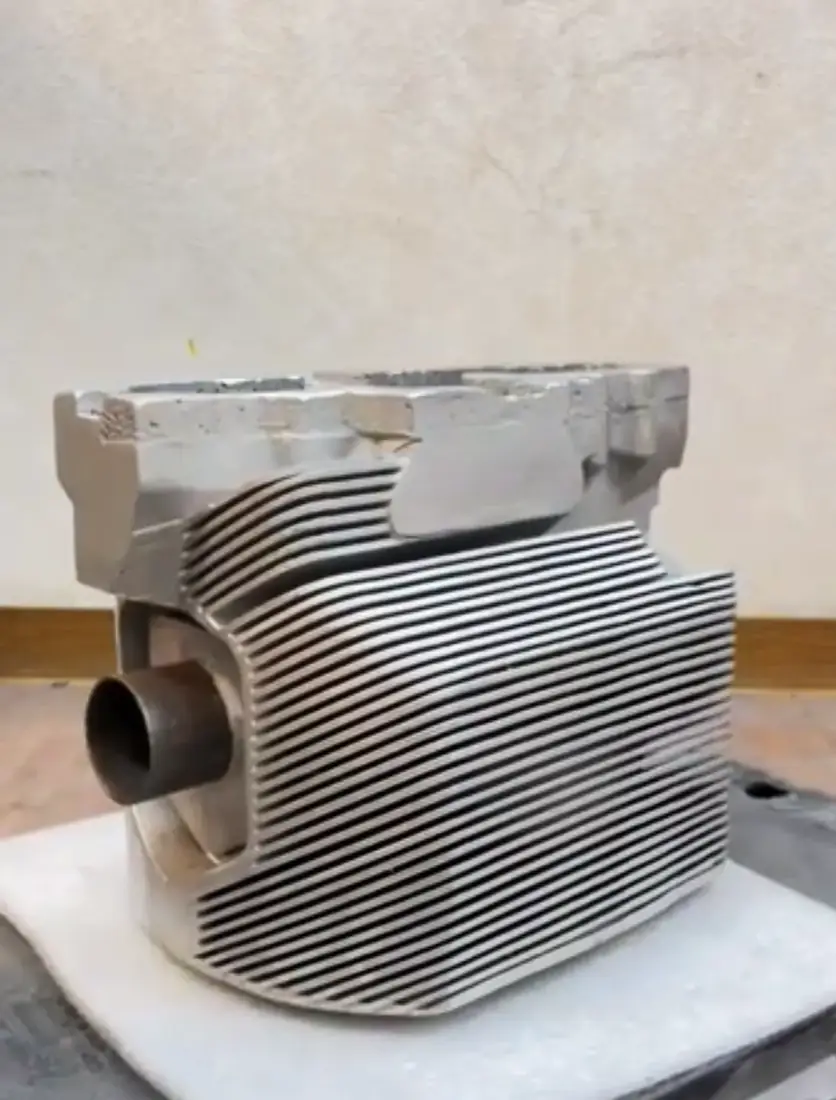
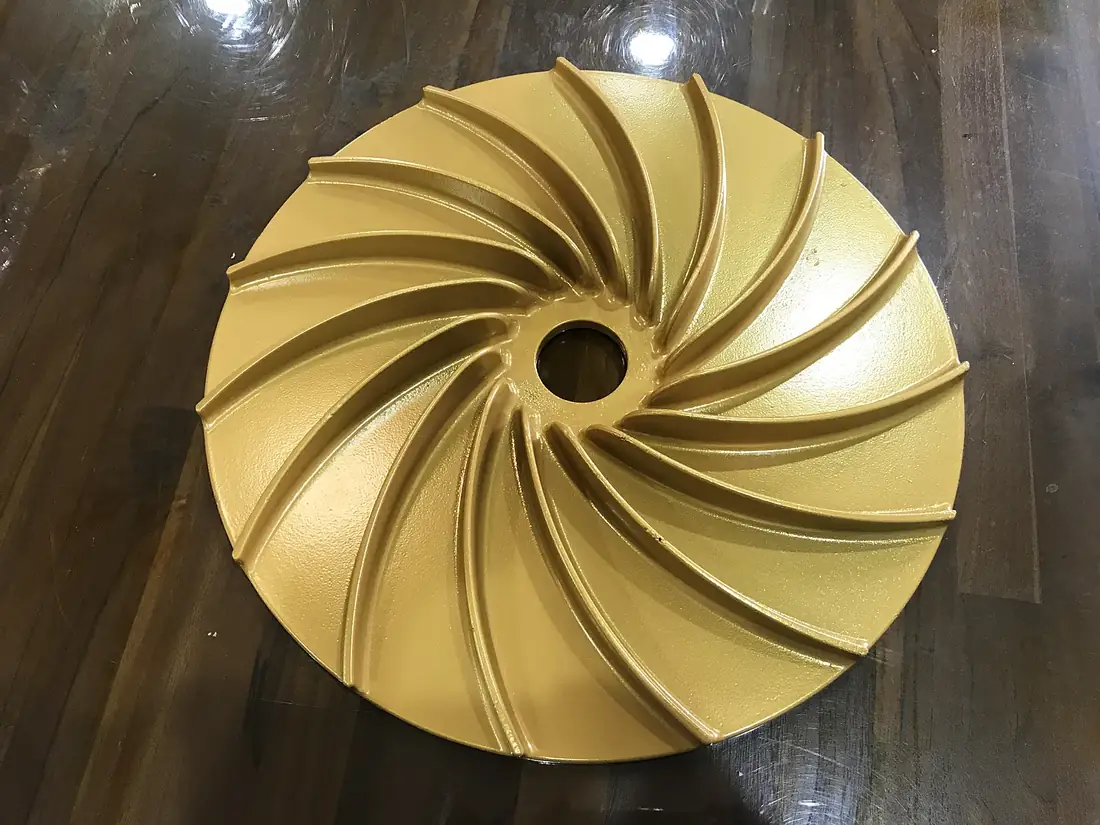
Why this matters: an internal spiral or serpentine channel cannot be drawn from a die, and cannot be machined in afterwards. A burned-out pattern leaves the cavity empty — so the channel is simply part of the casting.為什麼這件事重要:內部的螺旋或蛇形流道無法脫模,也無法事後加工進去。白模燒失之後型腔是空的 —— 流道就直接是鑄件的一部分。
What we can and cannot pour.我們澆得了什麼、澆不了什麼。
Straight numbers, so you can rule us in or out in thirty seconds.直接給數字,讓你三十秒內判斷要不要問我們。
| Parameter項目 | Value數值 |
|---|---|
| Alloy合金 | A356.2 (ZL101A) · T6 |
| Tensile strength, target抗拉強度(目標) | ≥ 280 MPa |
| Yield strength, target降伏強度(目標) | ≥ 210 MPa |
| Elongation, target延伸率(目標) | ≥ 8 % |
| Iron content鐵含量 | Fe ≤ 0.08 % |
| Max part envelope最大件尺寸 | On request依件洽詢 |
| Minimum wall最小壁厚 | On request依件洽詢 |
| As-cast tolerance鑄態公差 | On request依件洽詢 |
| As-cast surface鑄態表面粗糙度 | On request依件洽詢 |
| Process time, first piece製程時間(首件) | 5–10 days · excludes review, machining and shipping5~10 天 · 不含評估、加工與運送 |
| Tooling charge模具費 | None. Ever.沒有。一律沒有。 |
| Minimum order最低訂購量 | One piece一件起 |
The machining behind the casting.鑄件之後的那一段加工。
A raw casting is only half the part. Our machining partner is an IATF 16949 certified plant running 90 CNC machining centres across 11,000 m², with CMM and material spectrometer in-house and anodizing on the same site — so the part is finished, measured and surface-treated without leaving the supply chain.鑄件只是半成品。我們的合作加工廠通過 IATF 16949,擁有 90 台 CNC 加工中心、11,000 ㎡ 廠房,廠內配置三次元量測儀與材料光譜儀,並具備陽極氧化能力 —— 加工、量測、表面處理不必離開同一條供應鏈。
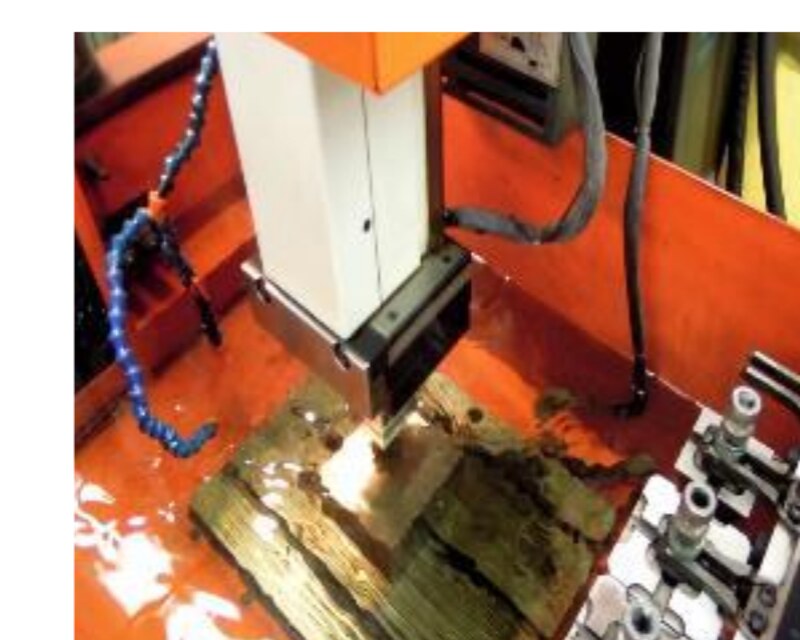
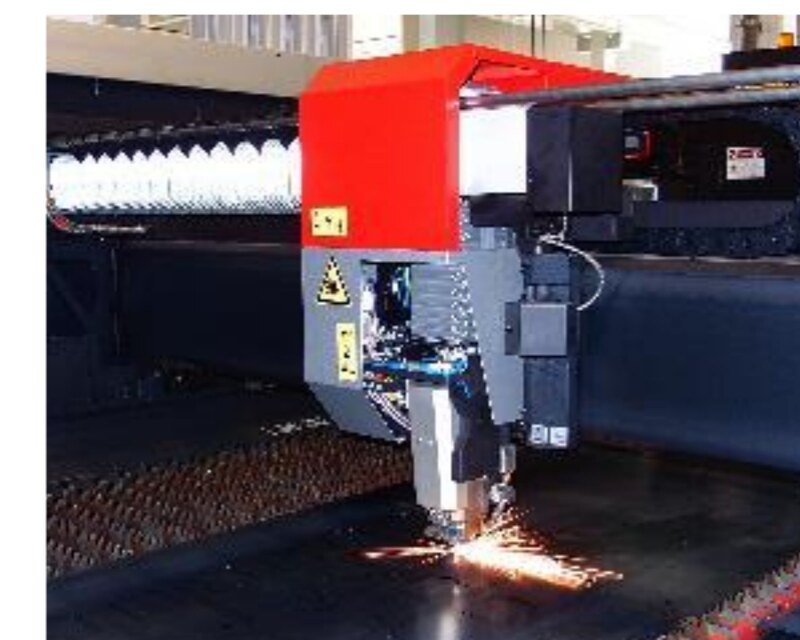
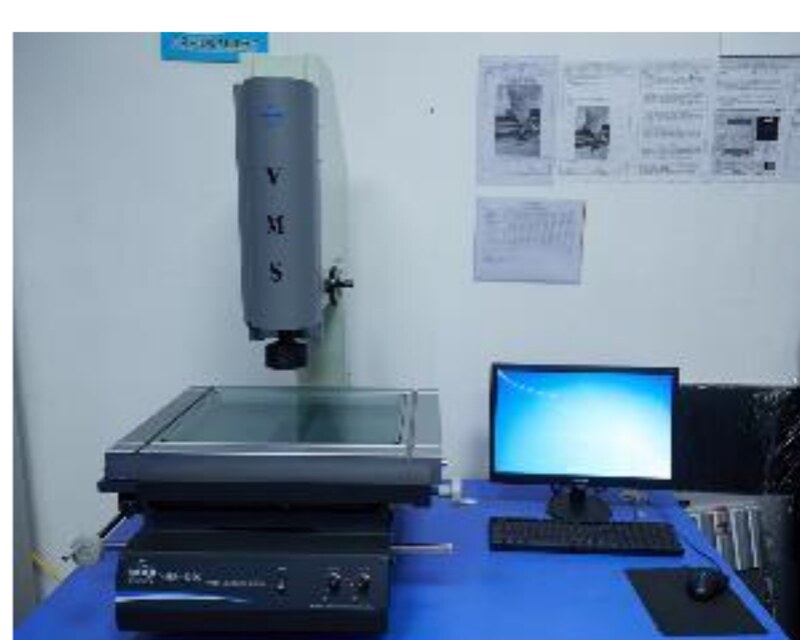
Why this matters: tooling-free casting removes the mould, not the tolerances. Datums, threads and critical surfaces still have to be machined and measured — and for automotive work the plant doing it has to be IATF 16949 certified. Ours is.為什麼重要:免開模拿掉的是模具,不是公差。基準面、螺紋與關鍵尺寸仍然要加工、要量測 —— 而車用件要求做這一段的工廠必須通過 IATF 16949。我們的合作廠有。
Four routes to a metal part, side by side.金屬鑄造產品生產技術分析。
Where this process sits: no tooling at all. Die casting, gravity casting, sand casting and investment casting all need a mould first — we don't. Lowest up-front investment, a minimum order of one, a process time on par with CNC, producing complex internal cavities and non-demouldable geometry, in the same metal as your production part.免開模快速鑄造的位置:完全不用開模具。壓鑄、重力鑄造、砂模、脫蠟都要先開模具 —— 我們不用。初期投入成本最低、最小訂購量為 1、製程時間與 CNC 同級,做得出複雜中空與無法脫模的幾何,用與量產件相同的金屬材料。
| Tooling-Free Rapid Casting免開模快速鑄造法 | Conventional casting通用鑄造法 | CNC machiningCNC 雕刻法 | Metal 3D printing金屬 3D 列印法 | |
|---|---|---|---|---|
| Process生產流程 | 1. 3D-print the polymer pattern 2. Coat it in ceramic slurry 3. Fire the pattern out at high heat 4. The same firing forms the shell 5. Pour molten metal into the shell 6. Break the shell off the casting1. 依照圖面 3D 列印塑料件 2. 將塑料件包裹陶瓷漿料 3. 高溫燒結將塑料液化 4. 高溫燒結同時形成陶瓷殼 5. 將金屬熔液注入空殼中 6. 將陶瓷殼去除取出鑄件 | 1. Cut the tool from the drawing 2. Set the tool in the machine 3. Apply release agent 4. Cast by pressure or gravity 5. Eject the casting from the tool ※ die, gravity, sand & investment casting all need a mould first1. 依照圖面製作模具 2. 將模具定位於設備 3. 塗上離型劑 4. 利用壓力或重力鑄造 5. 將鑄件從模具中取出 ※ 壓鑄・重力鑄造・砂模・脫蠟,皆須先開模具 | 1. Buy solid metal stock 2. Fixture the block in the CNC machine 3. Write the full CNC program 4. Remove the finished part1. 依照圖面購入金屬塊 2. 將金屬塊置於 CNC 設備 3. 編寫完整 CNC 程序加工 4. 加工完成後取下工件 | 1. Program the print from the file 2. Fuse powder layer by layer 3. Remove the part after sintering 4. Cut off the support structures1. 依照圖面編程列印程序 2. 設備一層一層燒結粉末 3. 燒結完成後取下工件 4. 將支撐腳去除完成工件 |
| Metals可用金屬 | Cast aluminium, cast iron, carbon steel, stainless steel, copper alloys鑄鋁、鑄鐵、碳鋼、不鏽鋼、銅 | Cast aluminium, cast iron, carbon steel, stainless steel, copper alloys鑄鋁、鑄鐵、碳鋼、不鏽鋼、銅 | Aluminium alloy, steel, stainless steel, copper alloys鋁合金、鋼、不鏽鋼、銅 | Aluminium alloy, titanium alloy鋁合金、鈦合金 |
| Process time (first piece)製程時間(首件) | 5–10 days5~10 天 | 120–150 days 90–120 tooling + 30 trial120~150 天 模具 90~120 + 試模 30 | 5–10 days5~10 天 | 2–7 days2~7 天 |
| Minimum order最小訂購量 | 11 | 1,000+1000 以上 | 11 | 11 |
| Cost per piece單件成本比較 | Medium中等 | Lowest最低 | High次高 | Highest最高 |
| Up-front investment初期投入成本 | Lowest最低 | Highest最高 | Medium中等 | High次高 |
| Best suited to適合的產品 | Complex hollow parts, parts that cannot be drawn from a mould, large castings, low volume / high mix, pre-tooling samples in the production spec, certification and approval samples matching that spec, parts that must be in the same metal as production複雜中空件、無法脫模件、大型鑄件、少量多樣、開模前同規格試樣件、需要與量產件同金屬材料、與量產件同規格之送驗品 | High volume, mature production批量大、成熟量產件 | Simple, precise small parts外型簡單且精密小型件 | Specialist alloys特殊材料件 |
Process time only. Every column is process time — it excludes castability review, downstream machining and shipping. The delivery date is confirmed per part at quotation.※ 各欄均為製程時間。不含可鑄性評估、後段機加工與運送;實際交期於報價時個案確認。
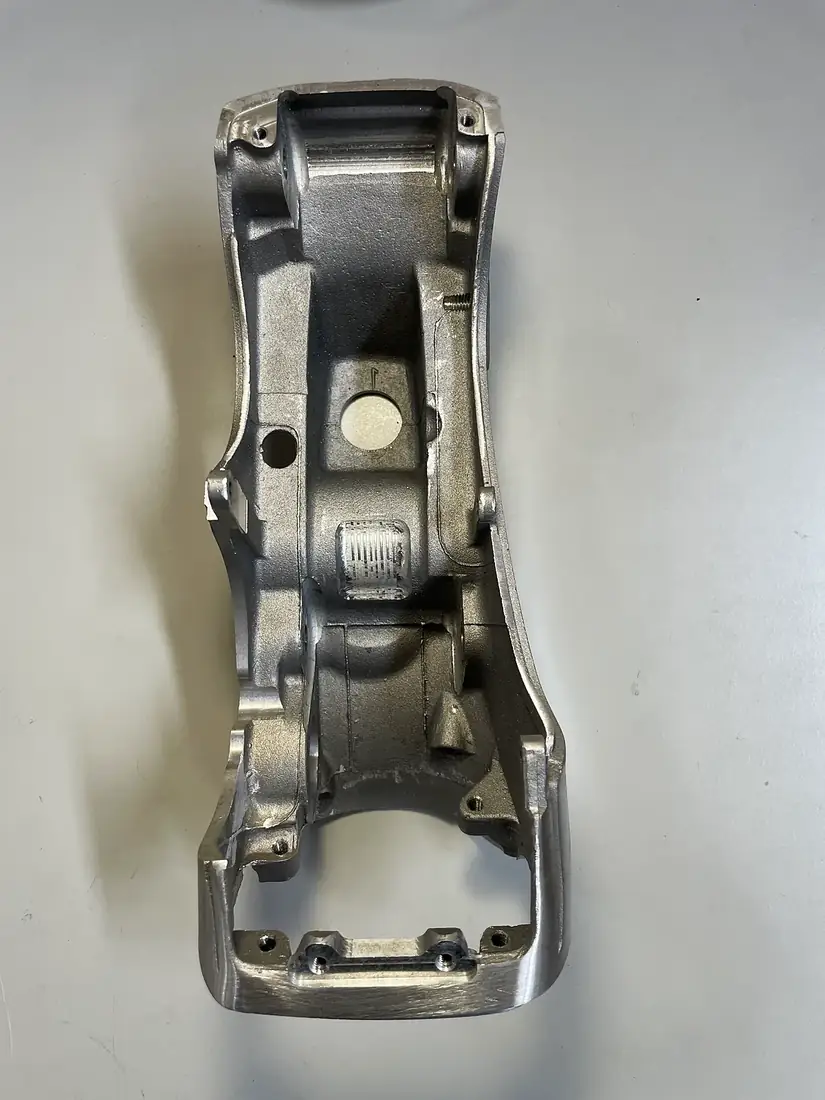
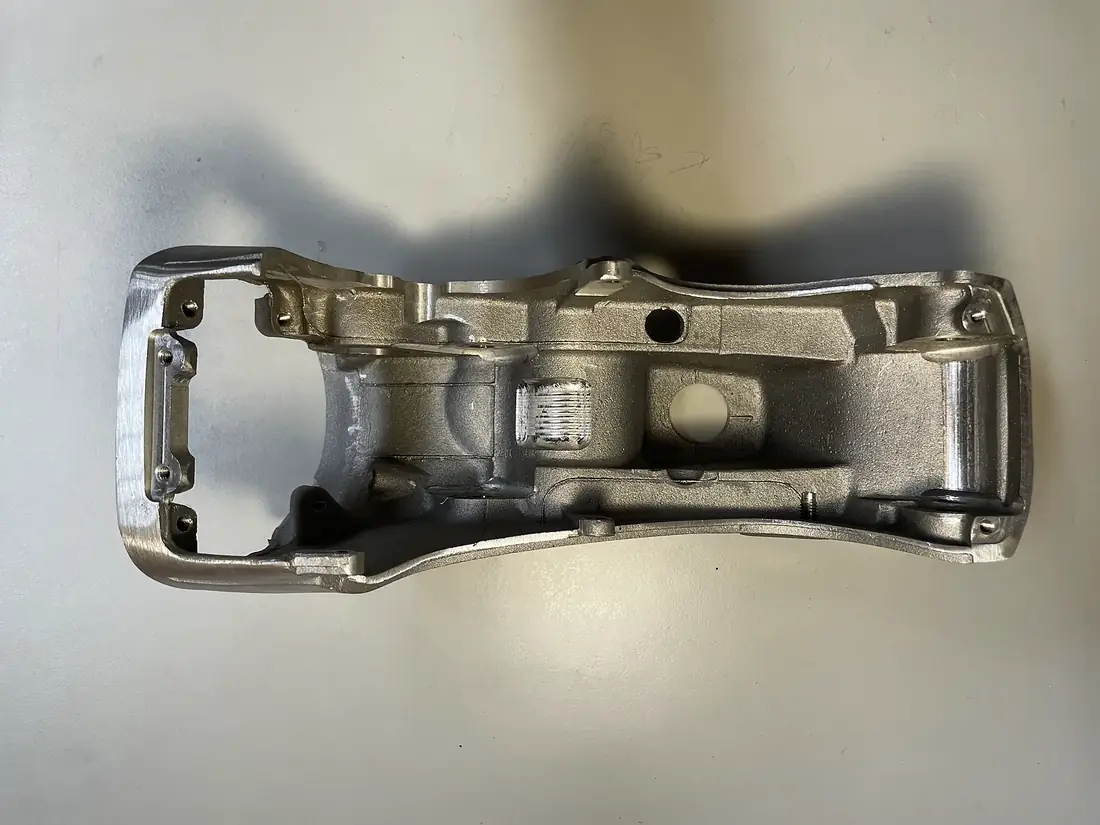
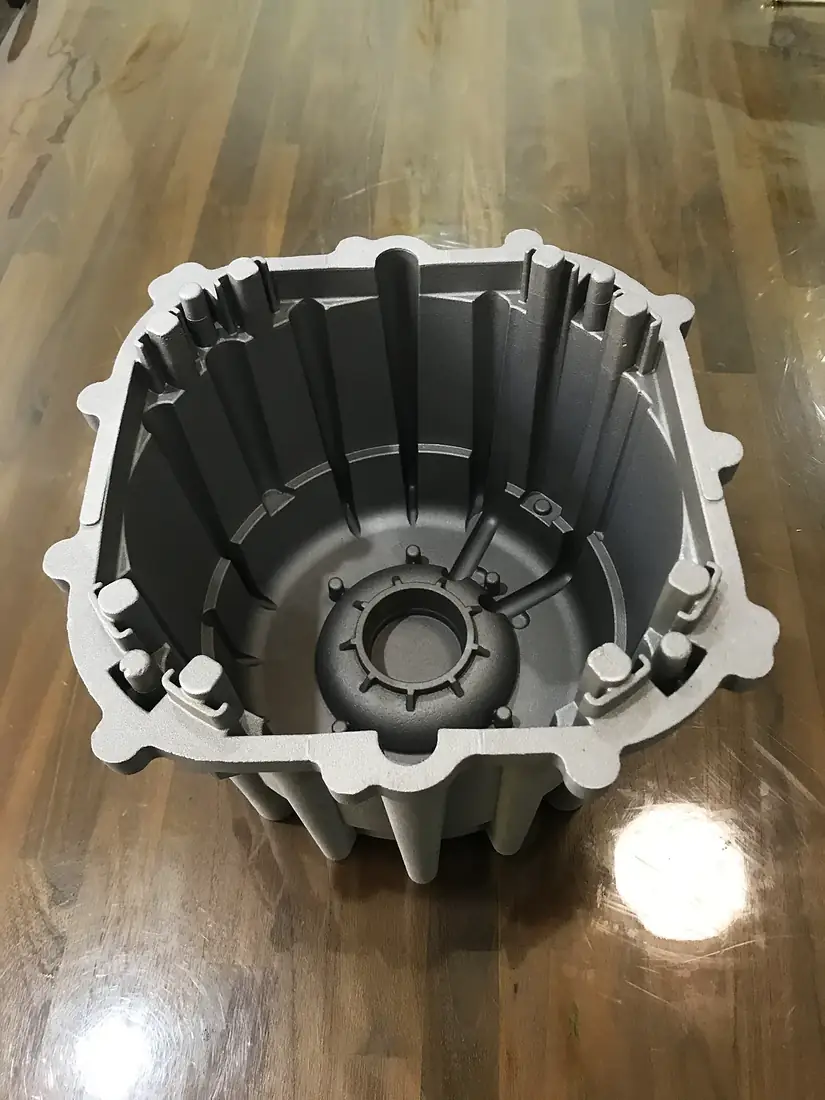
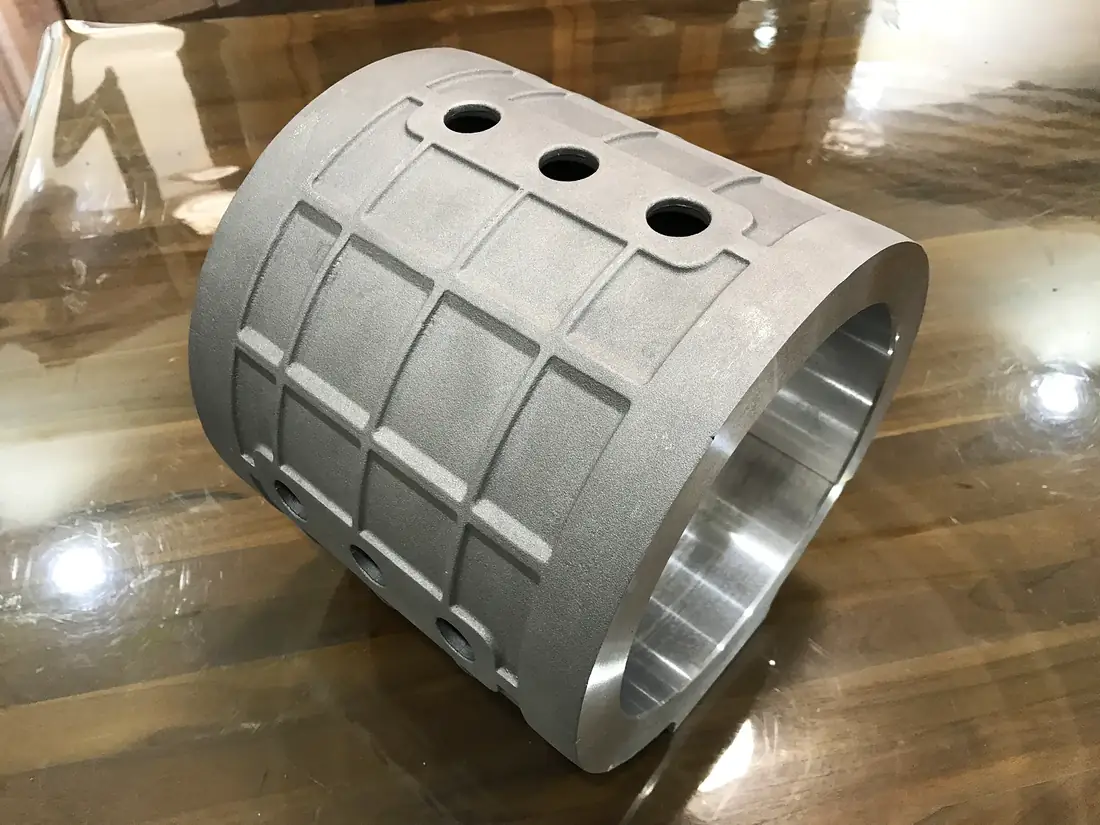
We would rather turn the job down than take it badly.不適合的案子,我們寧可不接。
Good fit適合
- You are about to commit to a die-casting or gravity tool and want the geometry proven first.
- 你正要下訂一套壓鑄模或重力模,想先把幾何驗過。
- Bridge production — you need parts now, the production tool is still being cut.
- 過渡量產 —— 現在就要件,但量產模具還在做。
- Volumes that will never justify a tool: spares, test rigs, special machinery, one-offs.
- 永遠不值得開模的量:備品、試驗治具、特殊機械、單件。
- Parts too large for the die-casting machine you have access to.
- 大件 —— 你找得到的壓鑄機噸位吃不下。
Poor fit不適合
- Thousands of pieces at a low unit price — go and open a tool, it will be cheaper.
- 幾千件、要低單價 —— 去開模,那樣便宜得多。
- Cosmetic parts where every surface must be machined anyway.
- 每一個面都要加工的外觀件 —— 那就直接 CNC。
- Anything needing a certified fatigue life from us. We supply data, not a warranty.
- 要我們背疲勞壽命保證的件。我們提供數據,不提供保證。
- Steel, stainless or magnesium. Aluminium only.
- 鋼、不鏽鋼、鎂合金。我們只做鋁。
A working foundry, not a render.是真的在跑的產線,不是算圖。
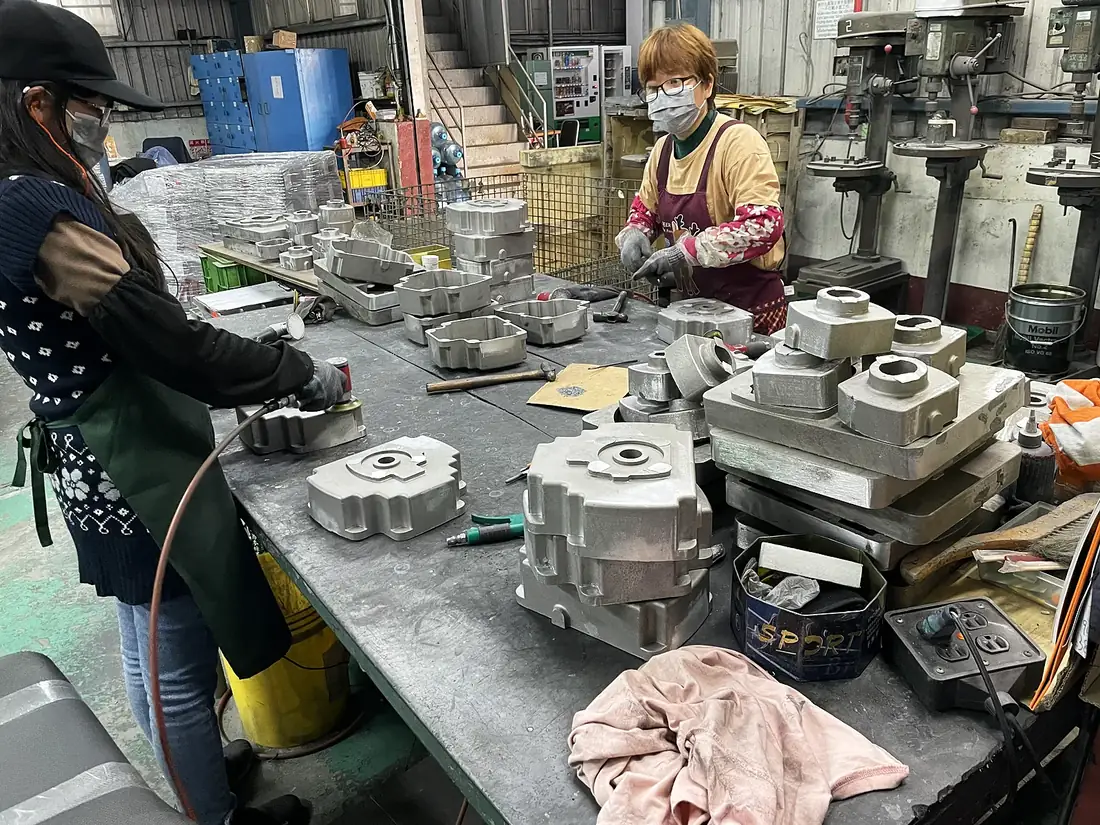
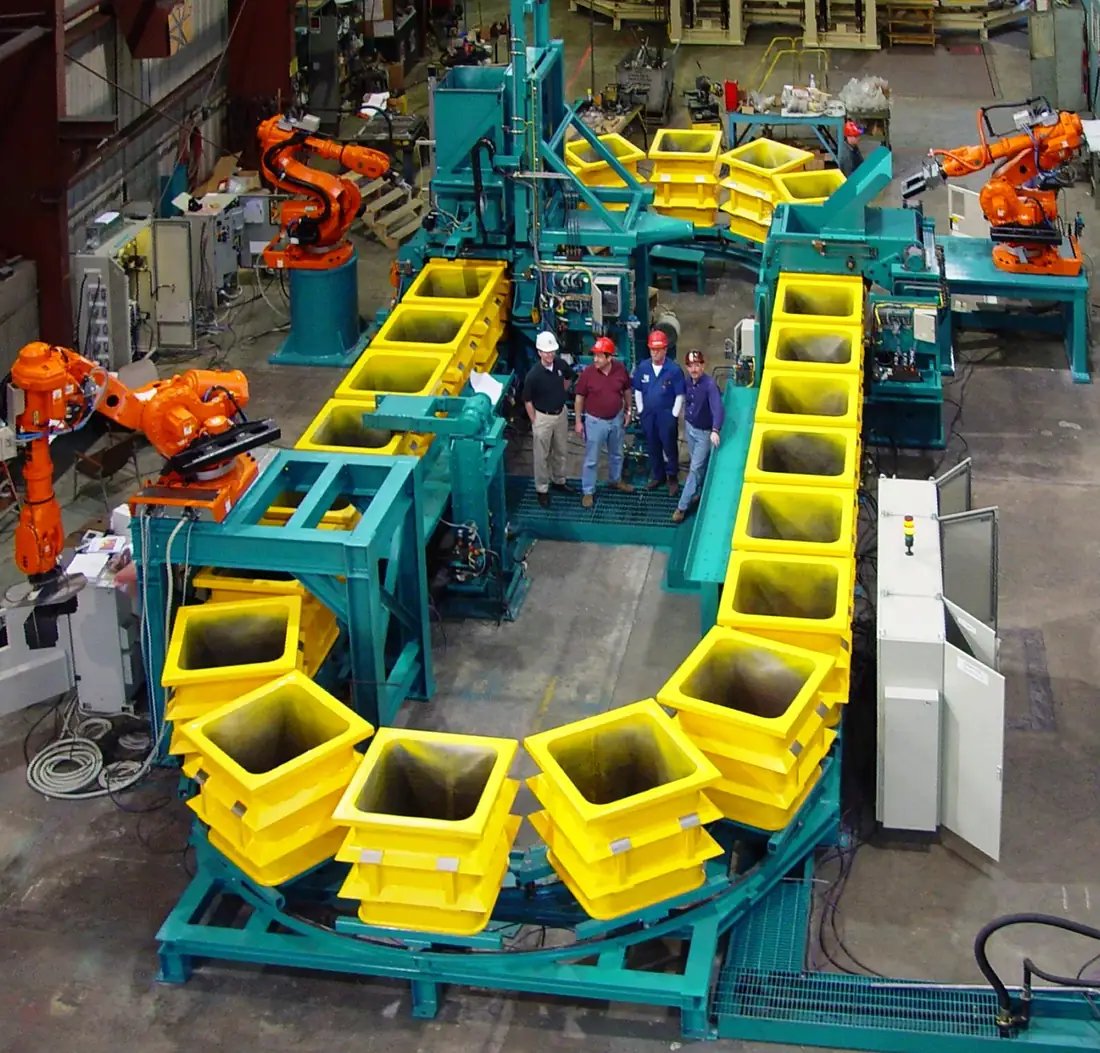
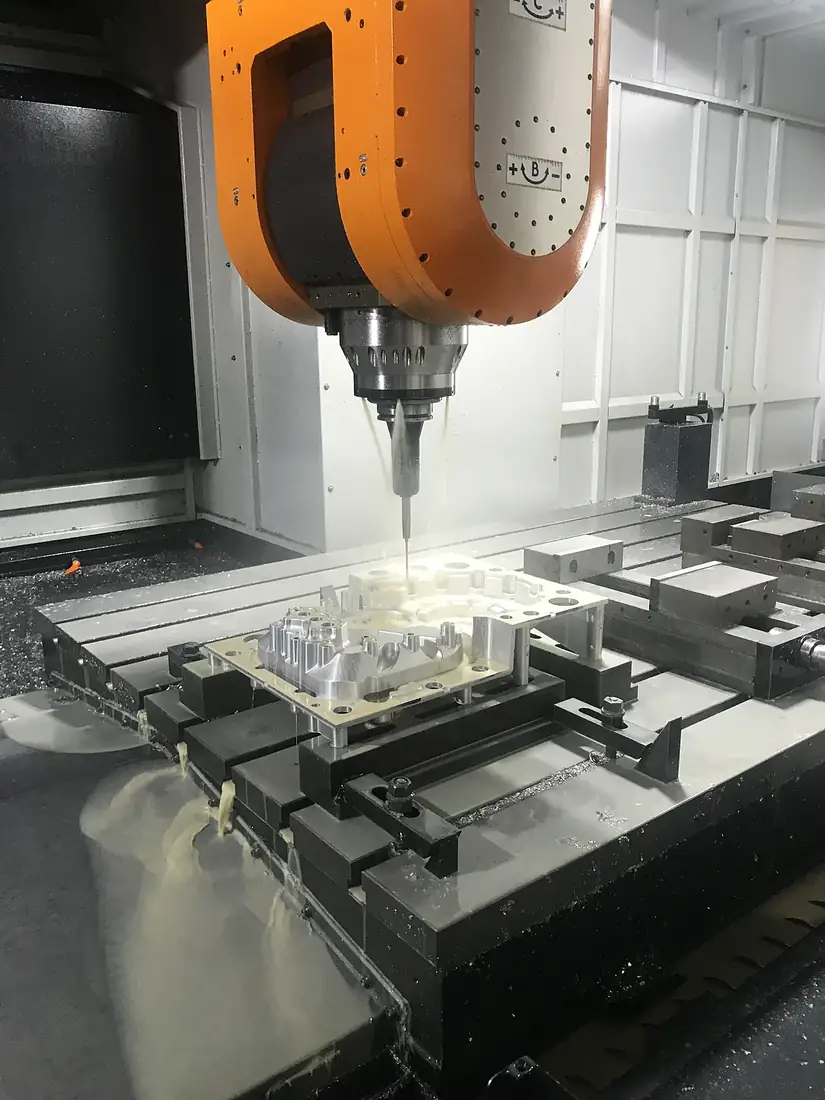
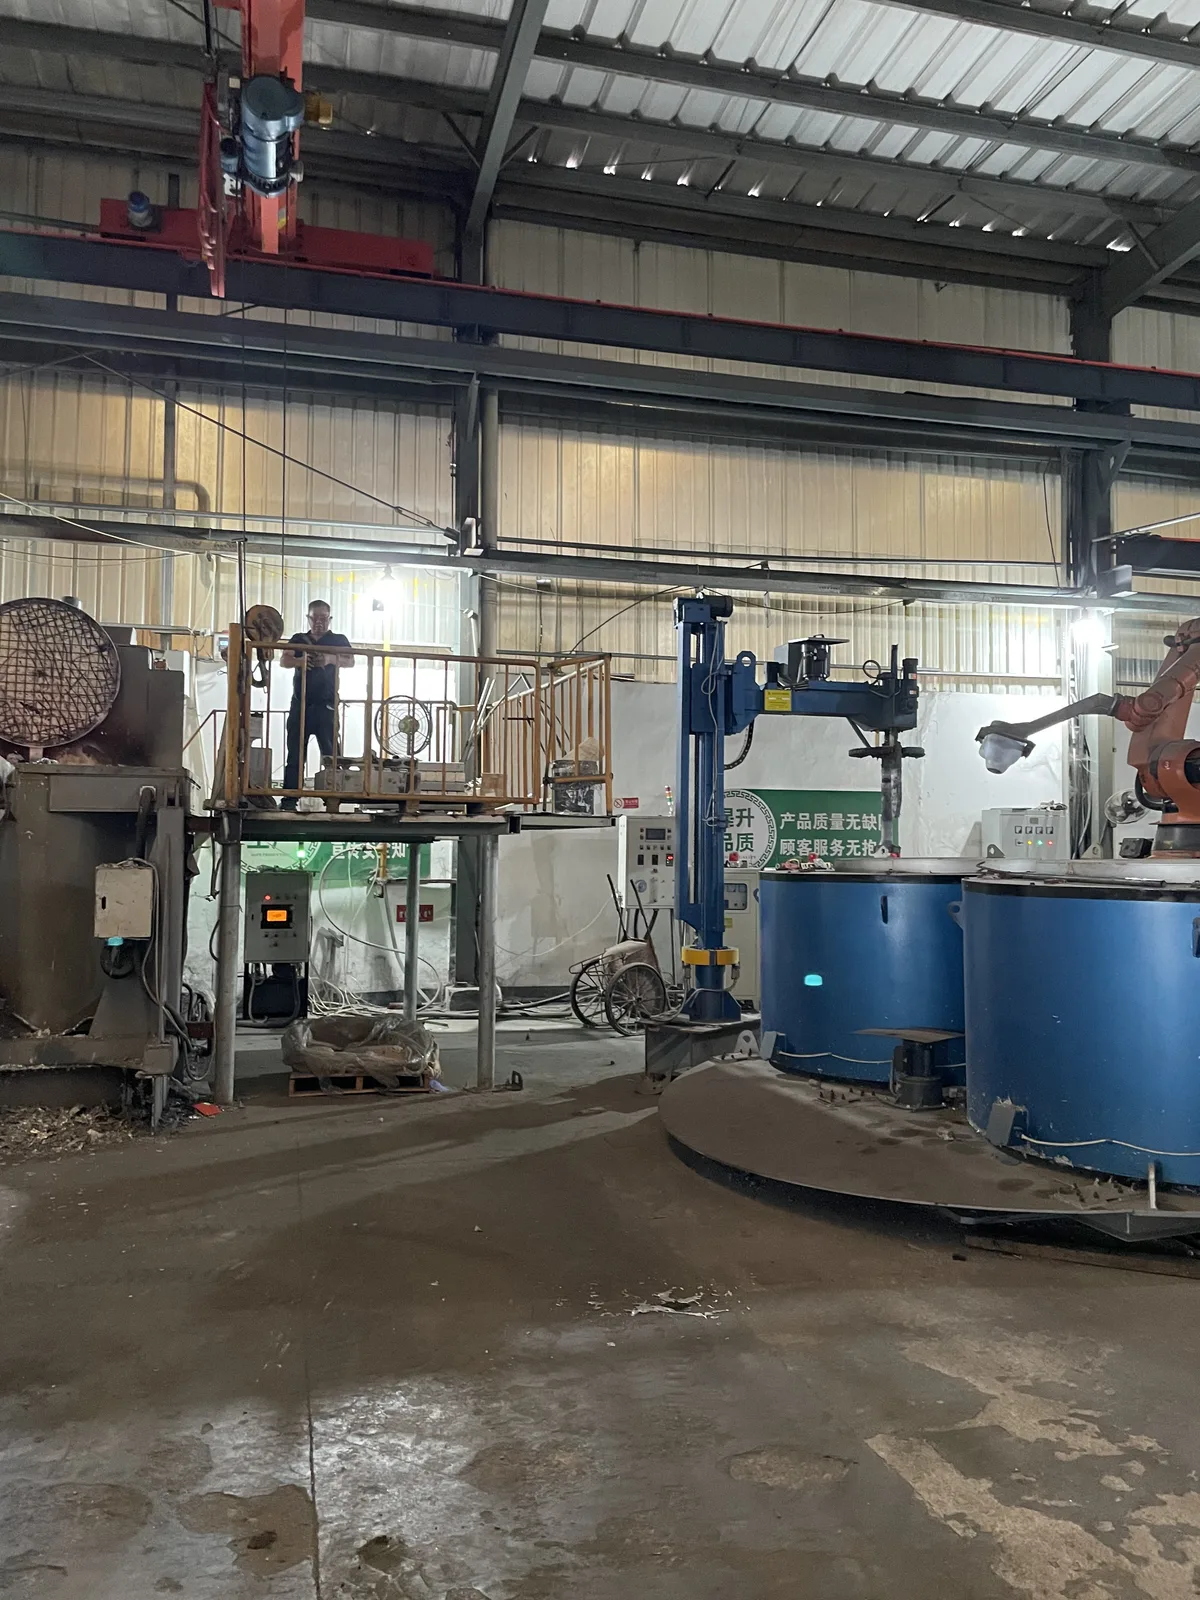
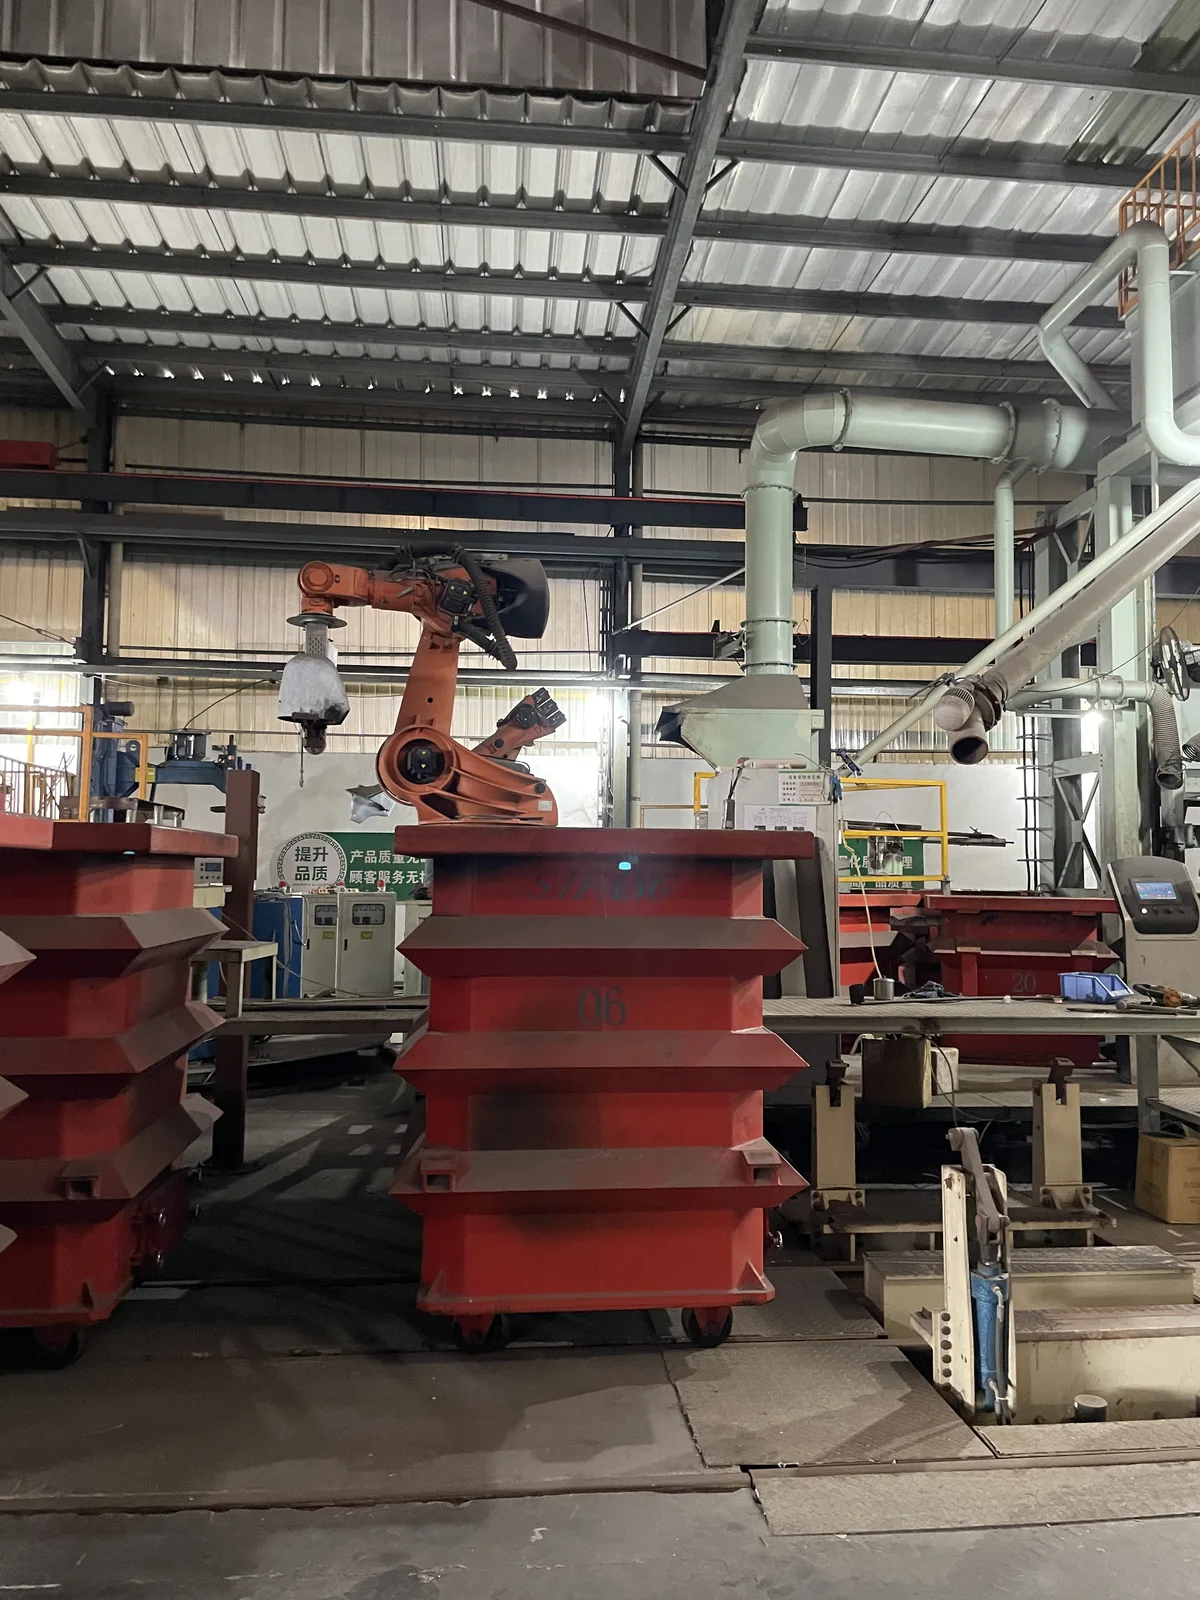
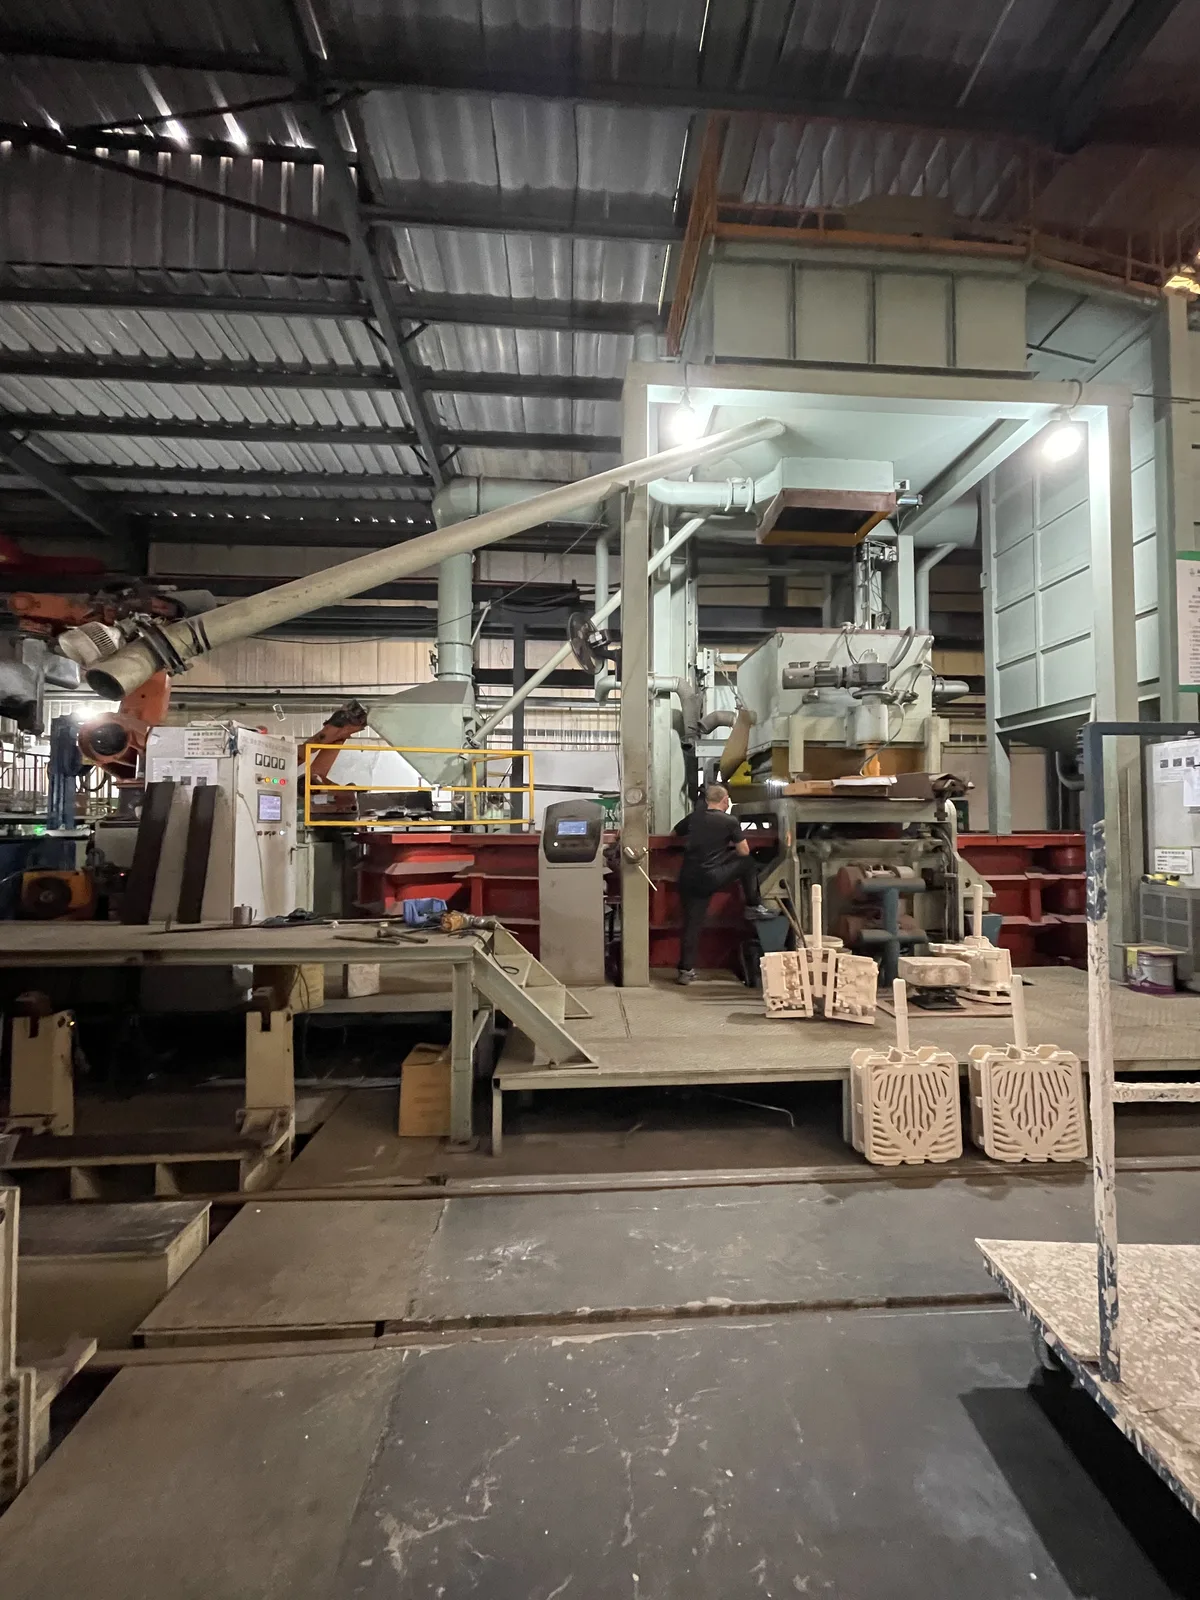
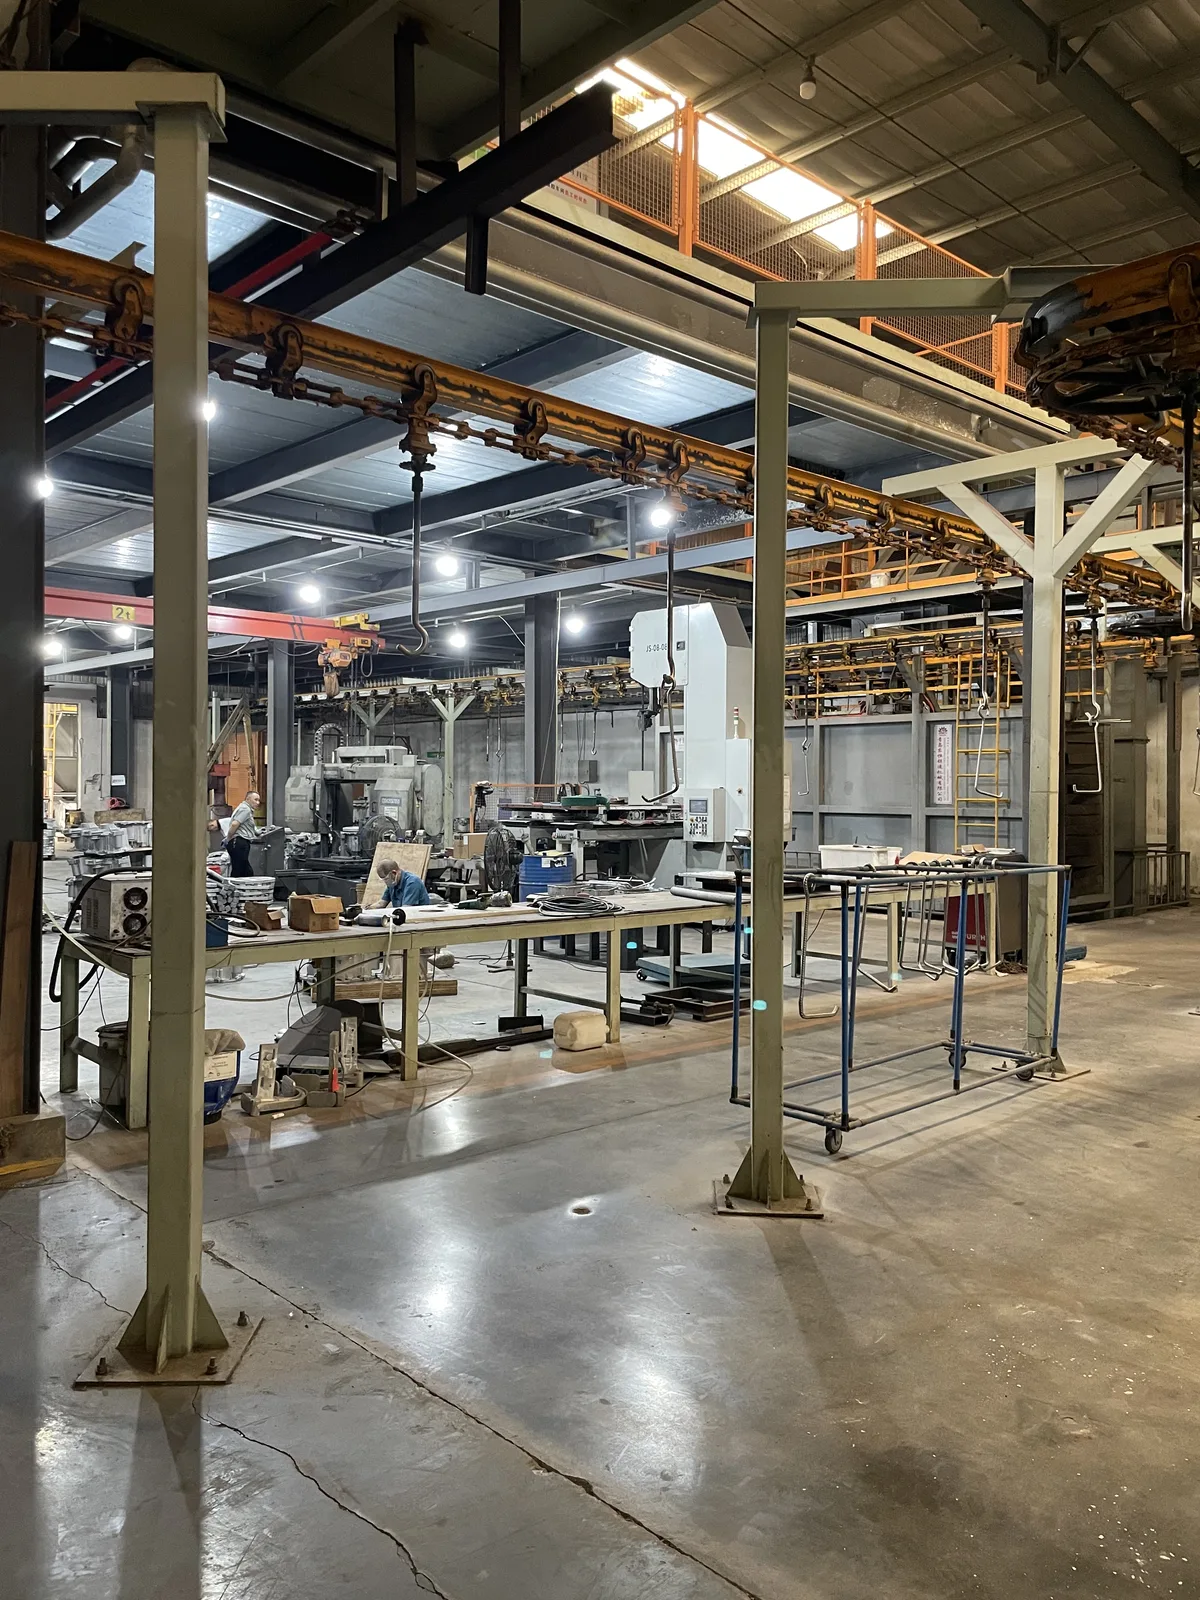
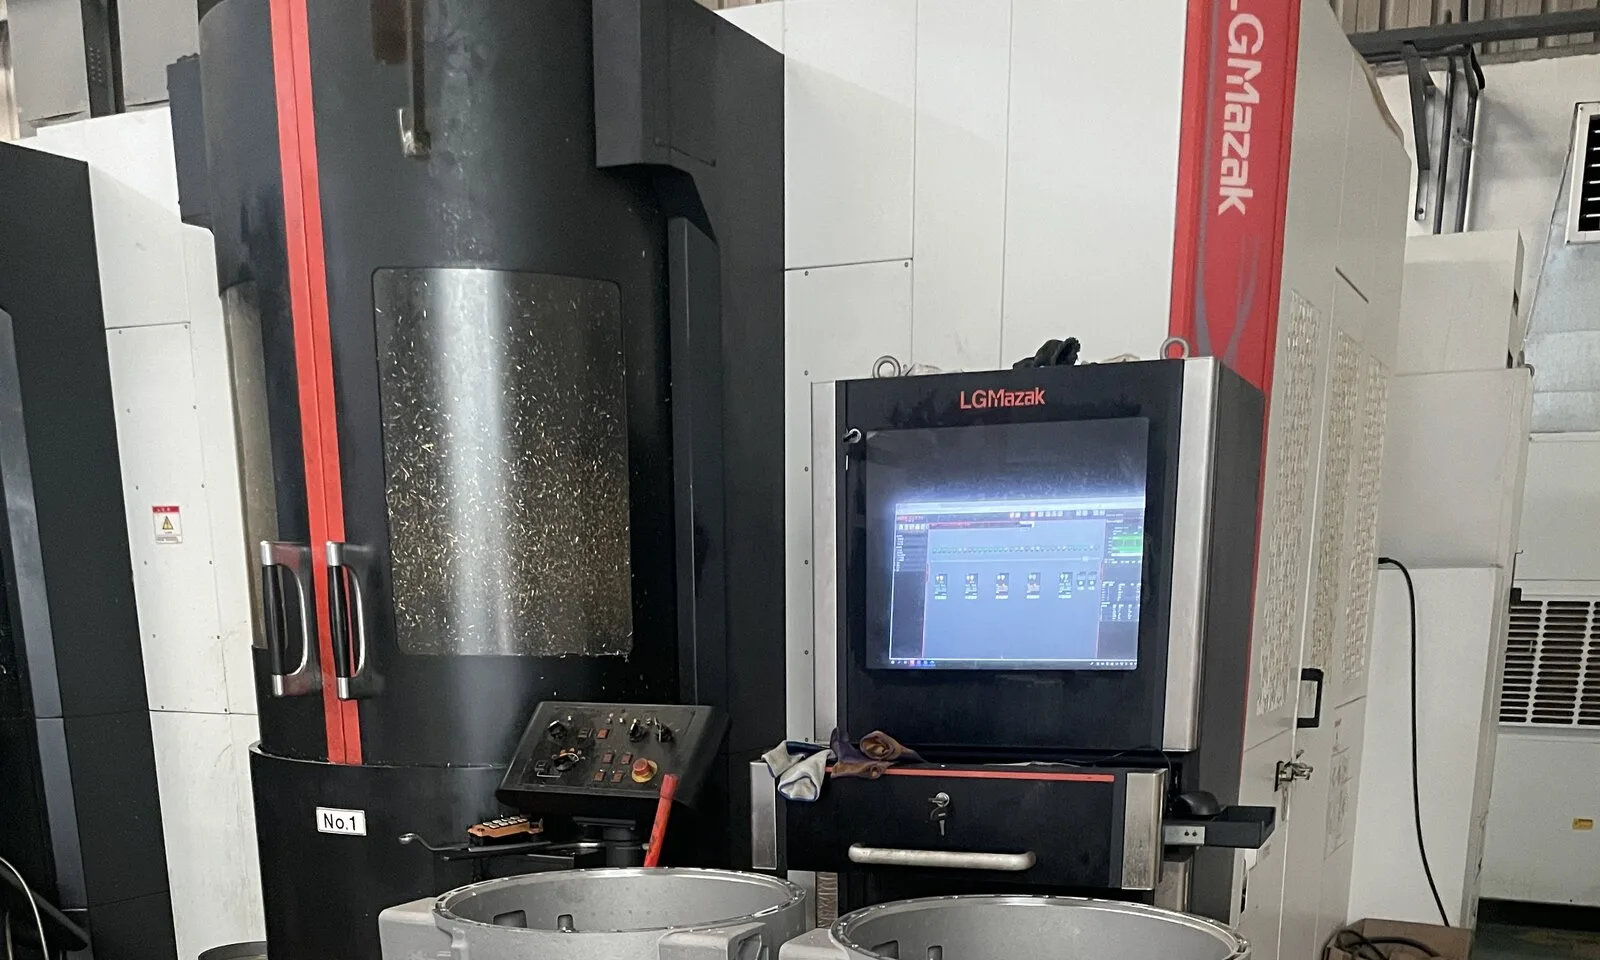
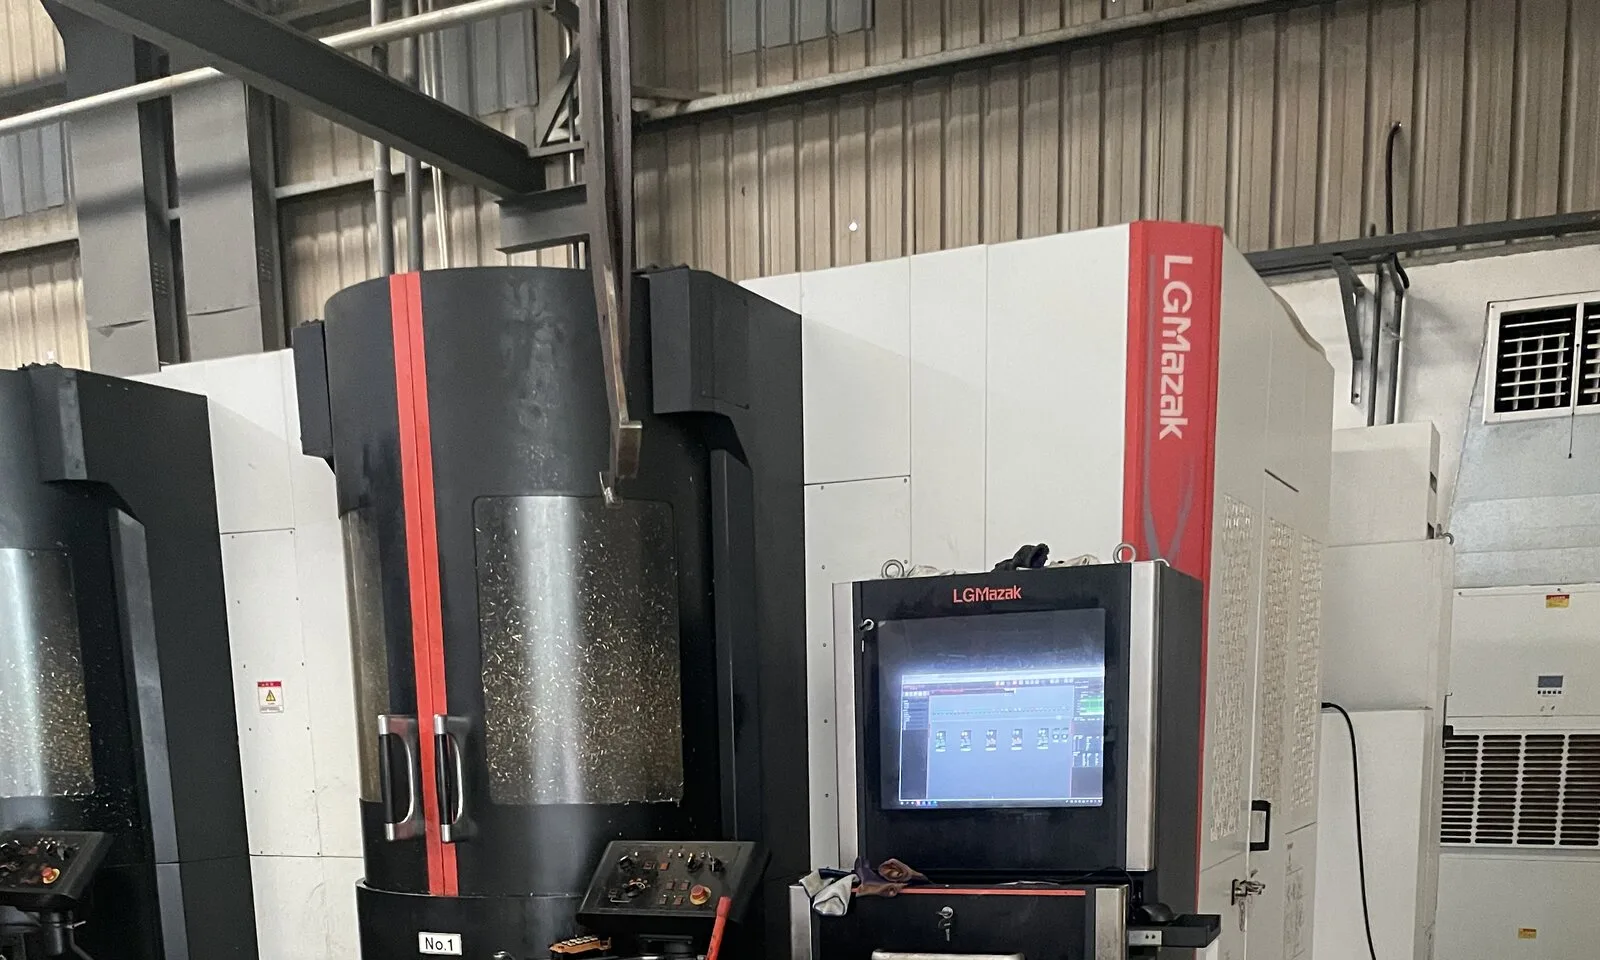
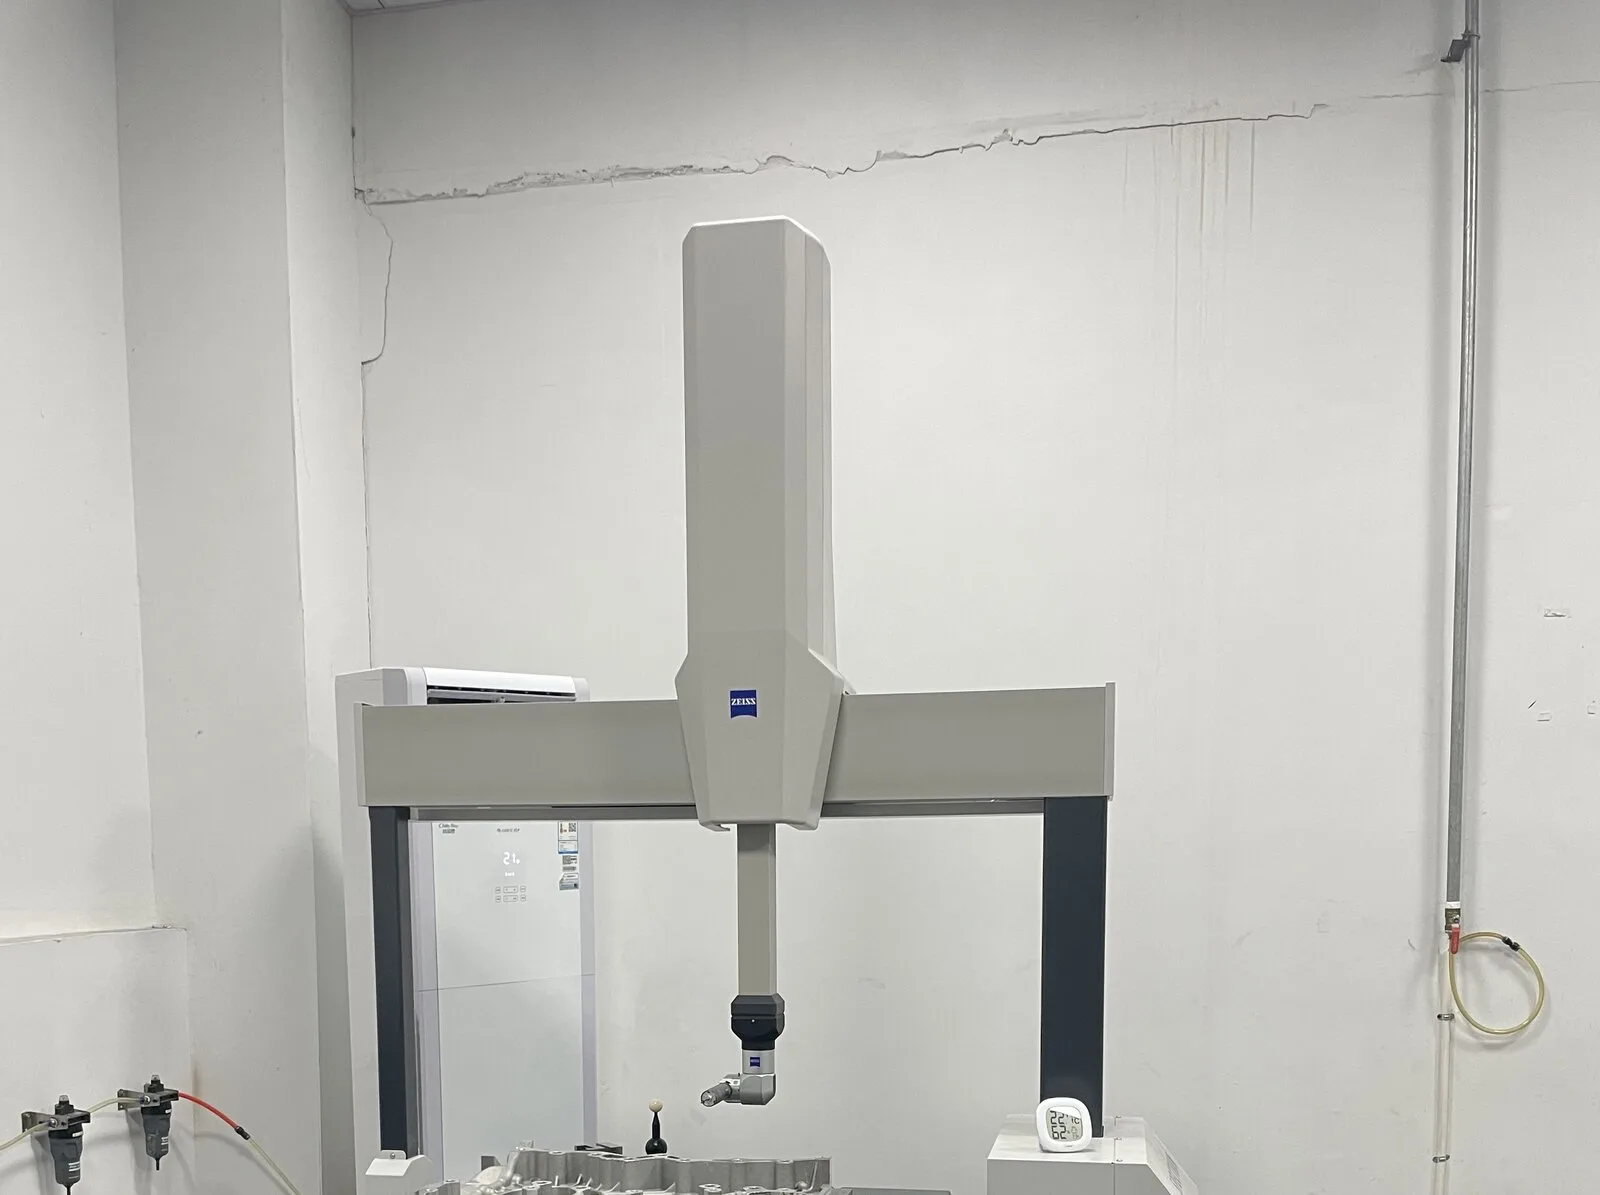
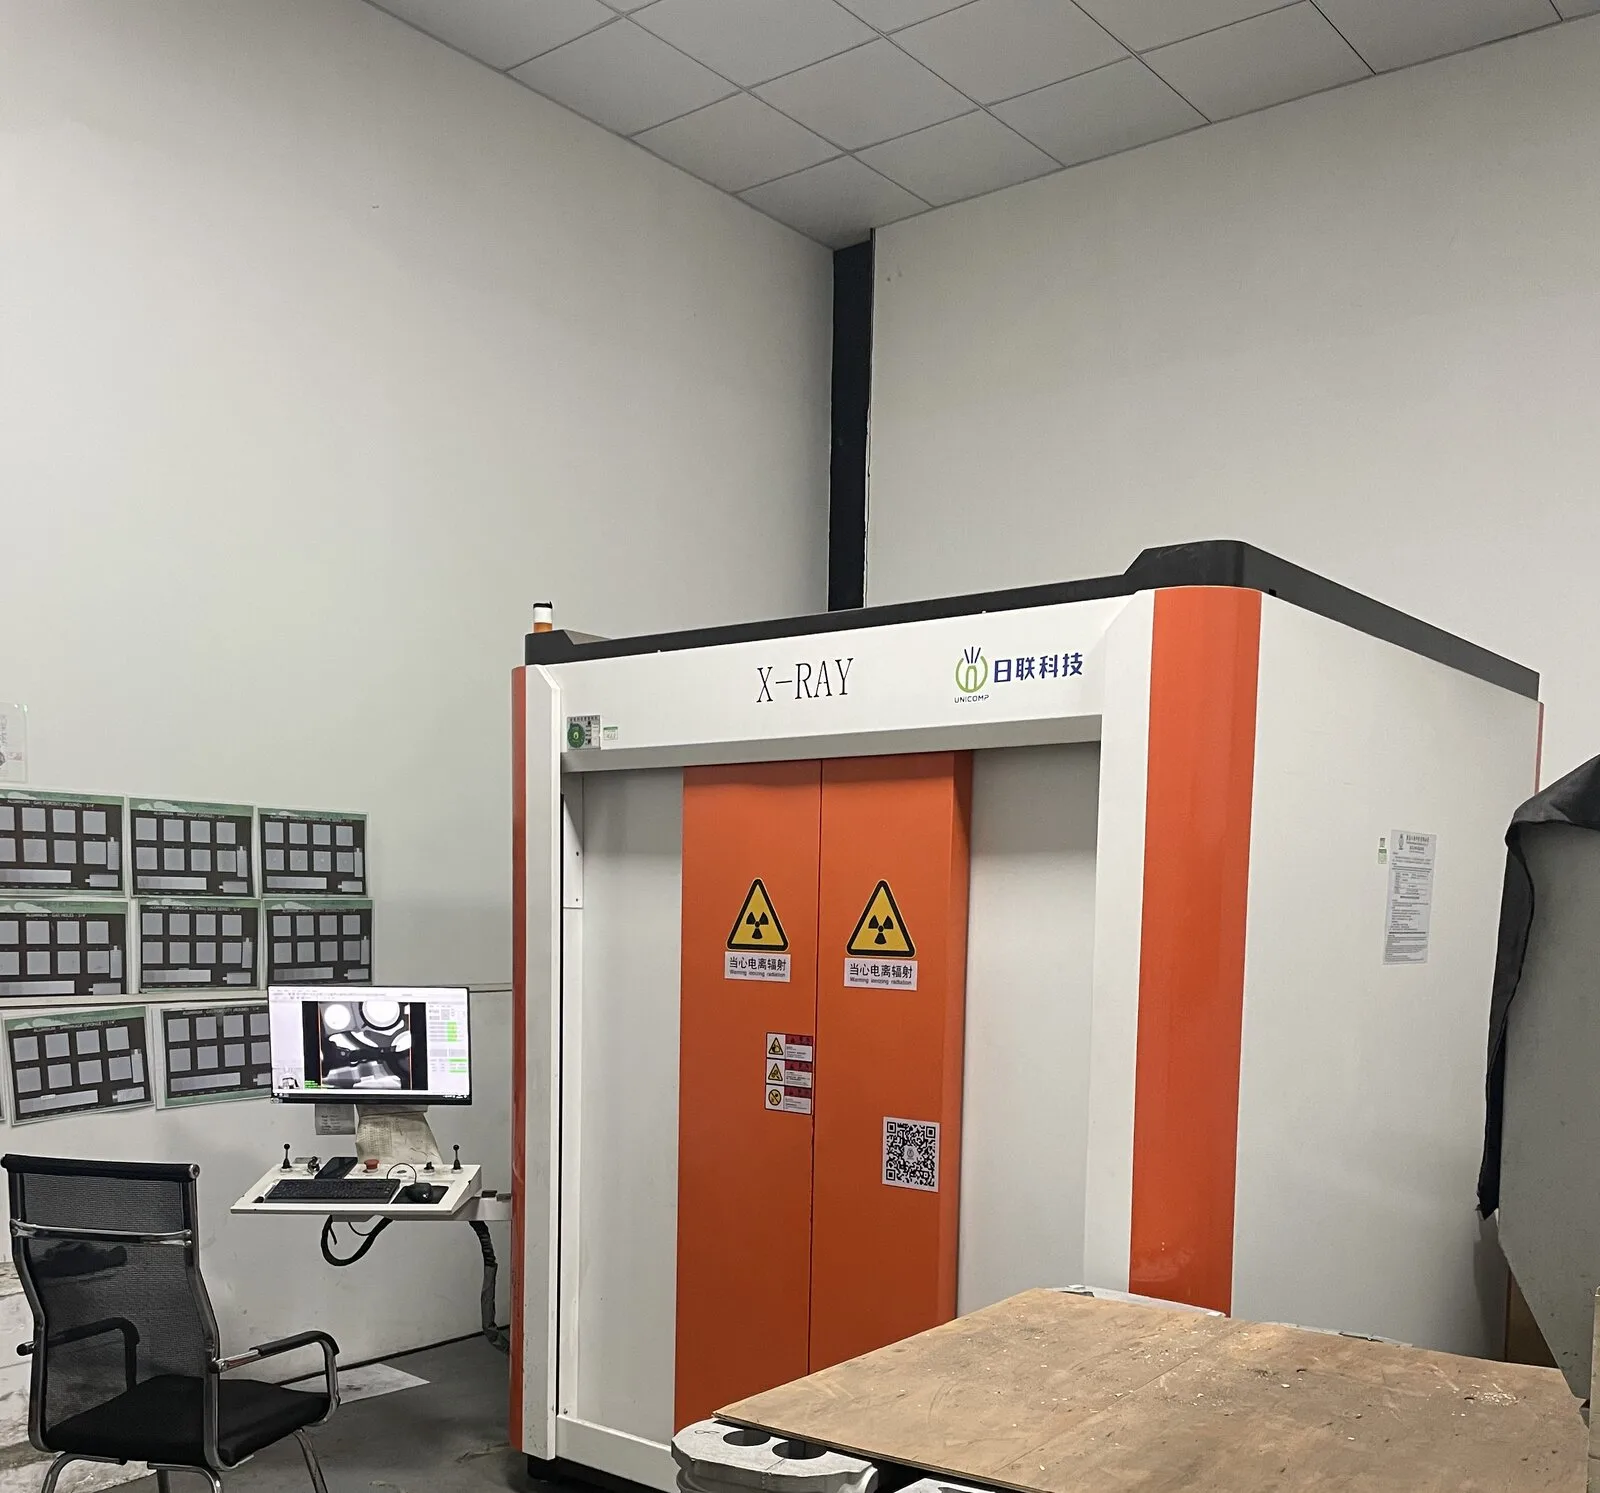
The full shell-mould process, start to finish.殼型鑄造的完整工藝流程。
Ten stages. Stages 03–05 are what make it a shell process: the pattern is liquefied out, then fired into a ceramic shell — so the cavity is completely empty when the metal arrives.十個工序。其中 03~05 是「殼型」的關鍵 —— 白模先液化流出,再高溫焙燒成陶瓷空殼,所以澆鑄時型腔完全是空的。
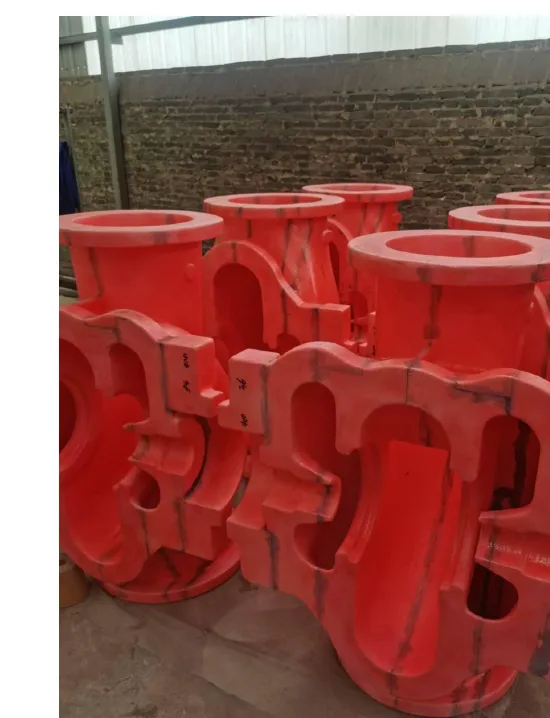
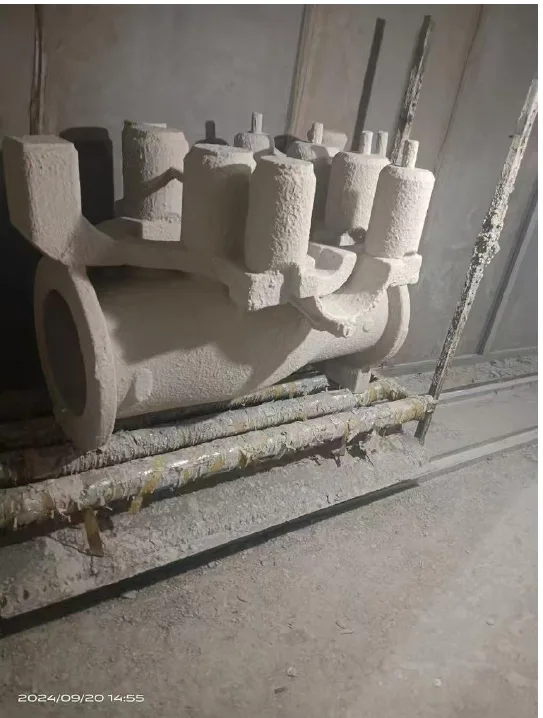
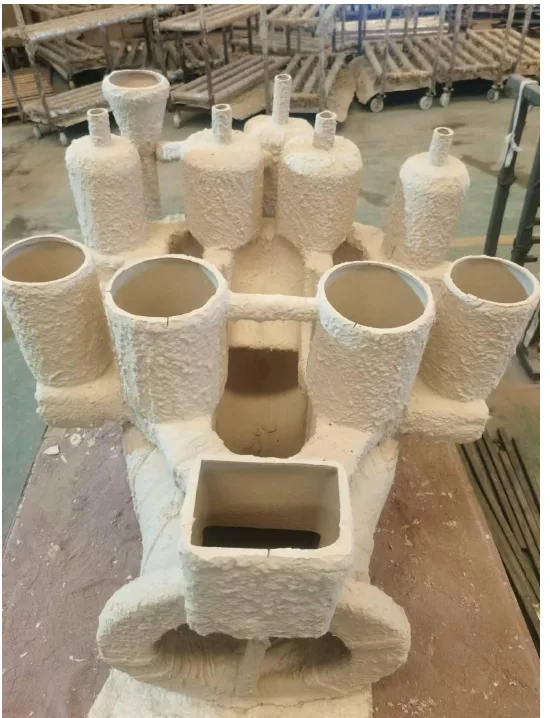
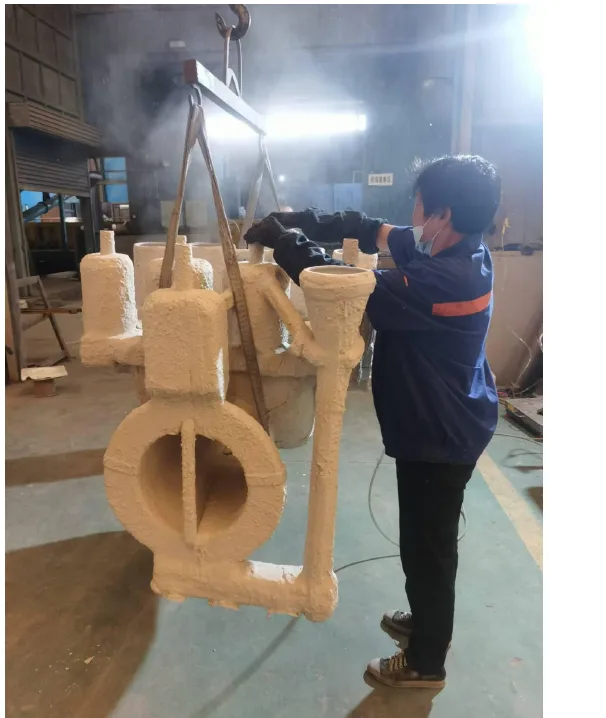
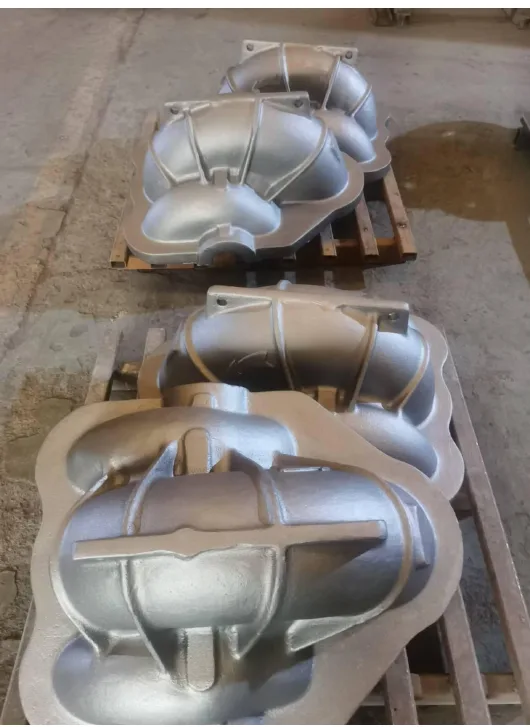
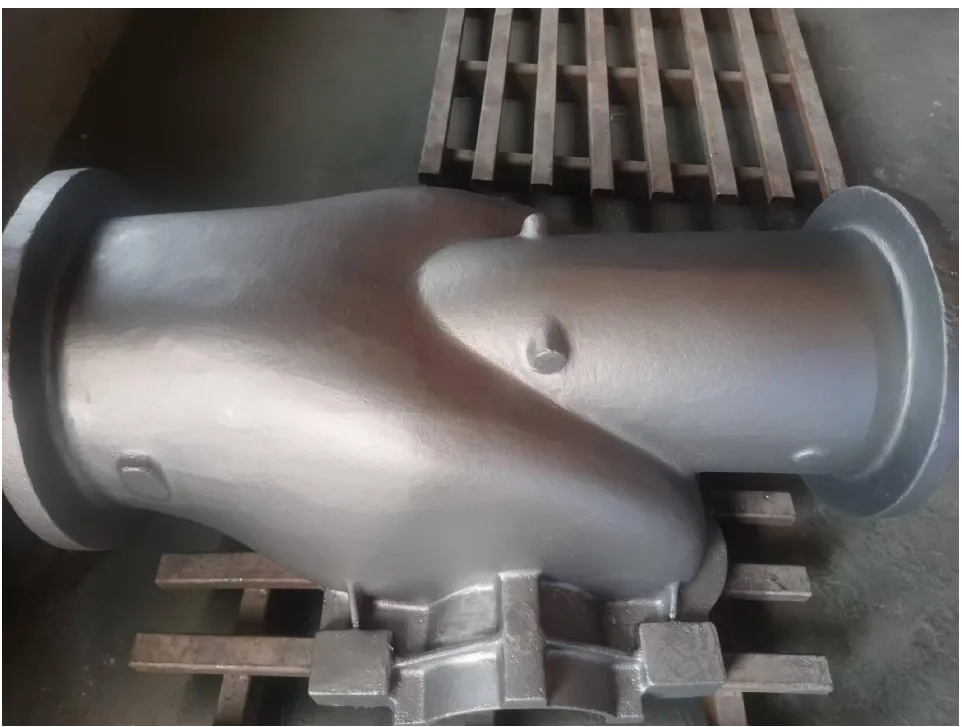
Photographs from the production line we work with. The parts shown are steel and stainless castings in the 20–2000 kg range — they illustrate the process, not our own product range.照片攝於合作產線。圖中為 20–2000 kg 級的鋼/不鏽鋼鑄件,用以說明工藝本身,非本公司的產品範圍。
Send the file. We answer within one working day.把檔案傳過來,一個工作日內回覆。
No account, no sales call. A real engineer reads the file and tells you whether it can be cast, what it costs, and how long it takes.不用註冊、不會有業務電話。由懂鑄造的人親自看檔案,告訴你這件鑄不鑄得出來、多少錢、要多久。